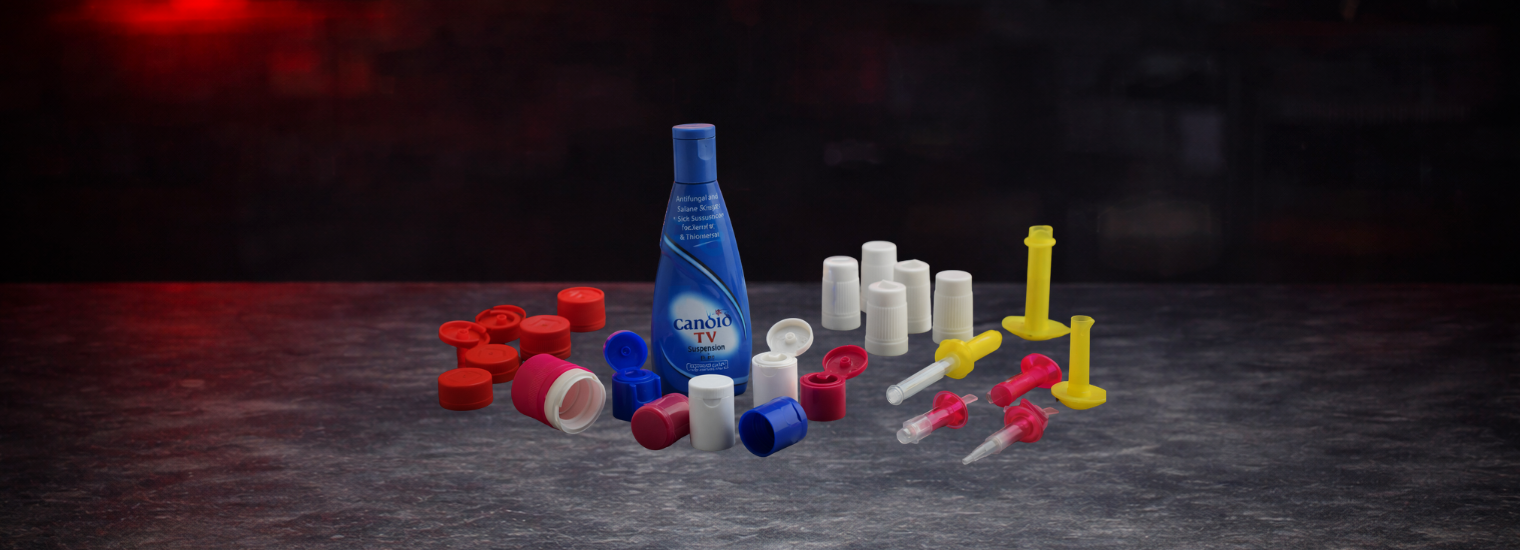
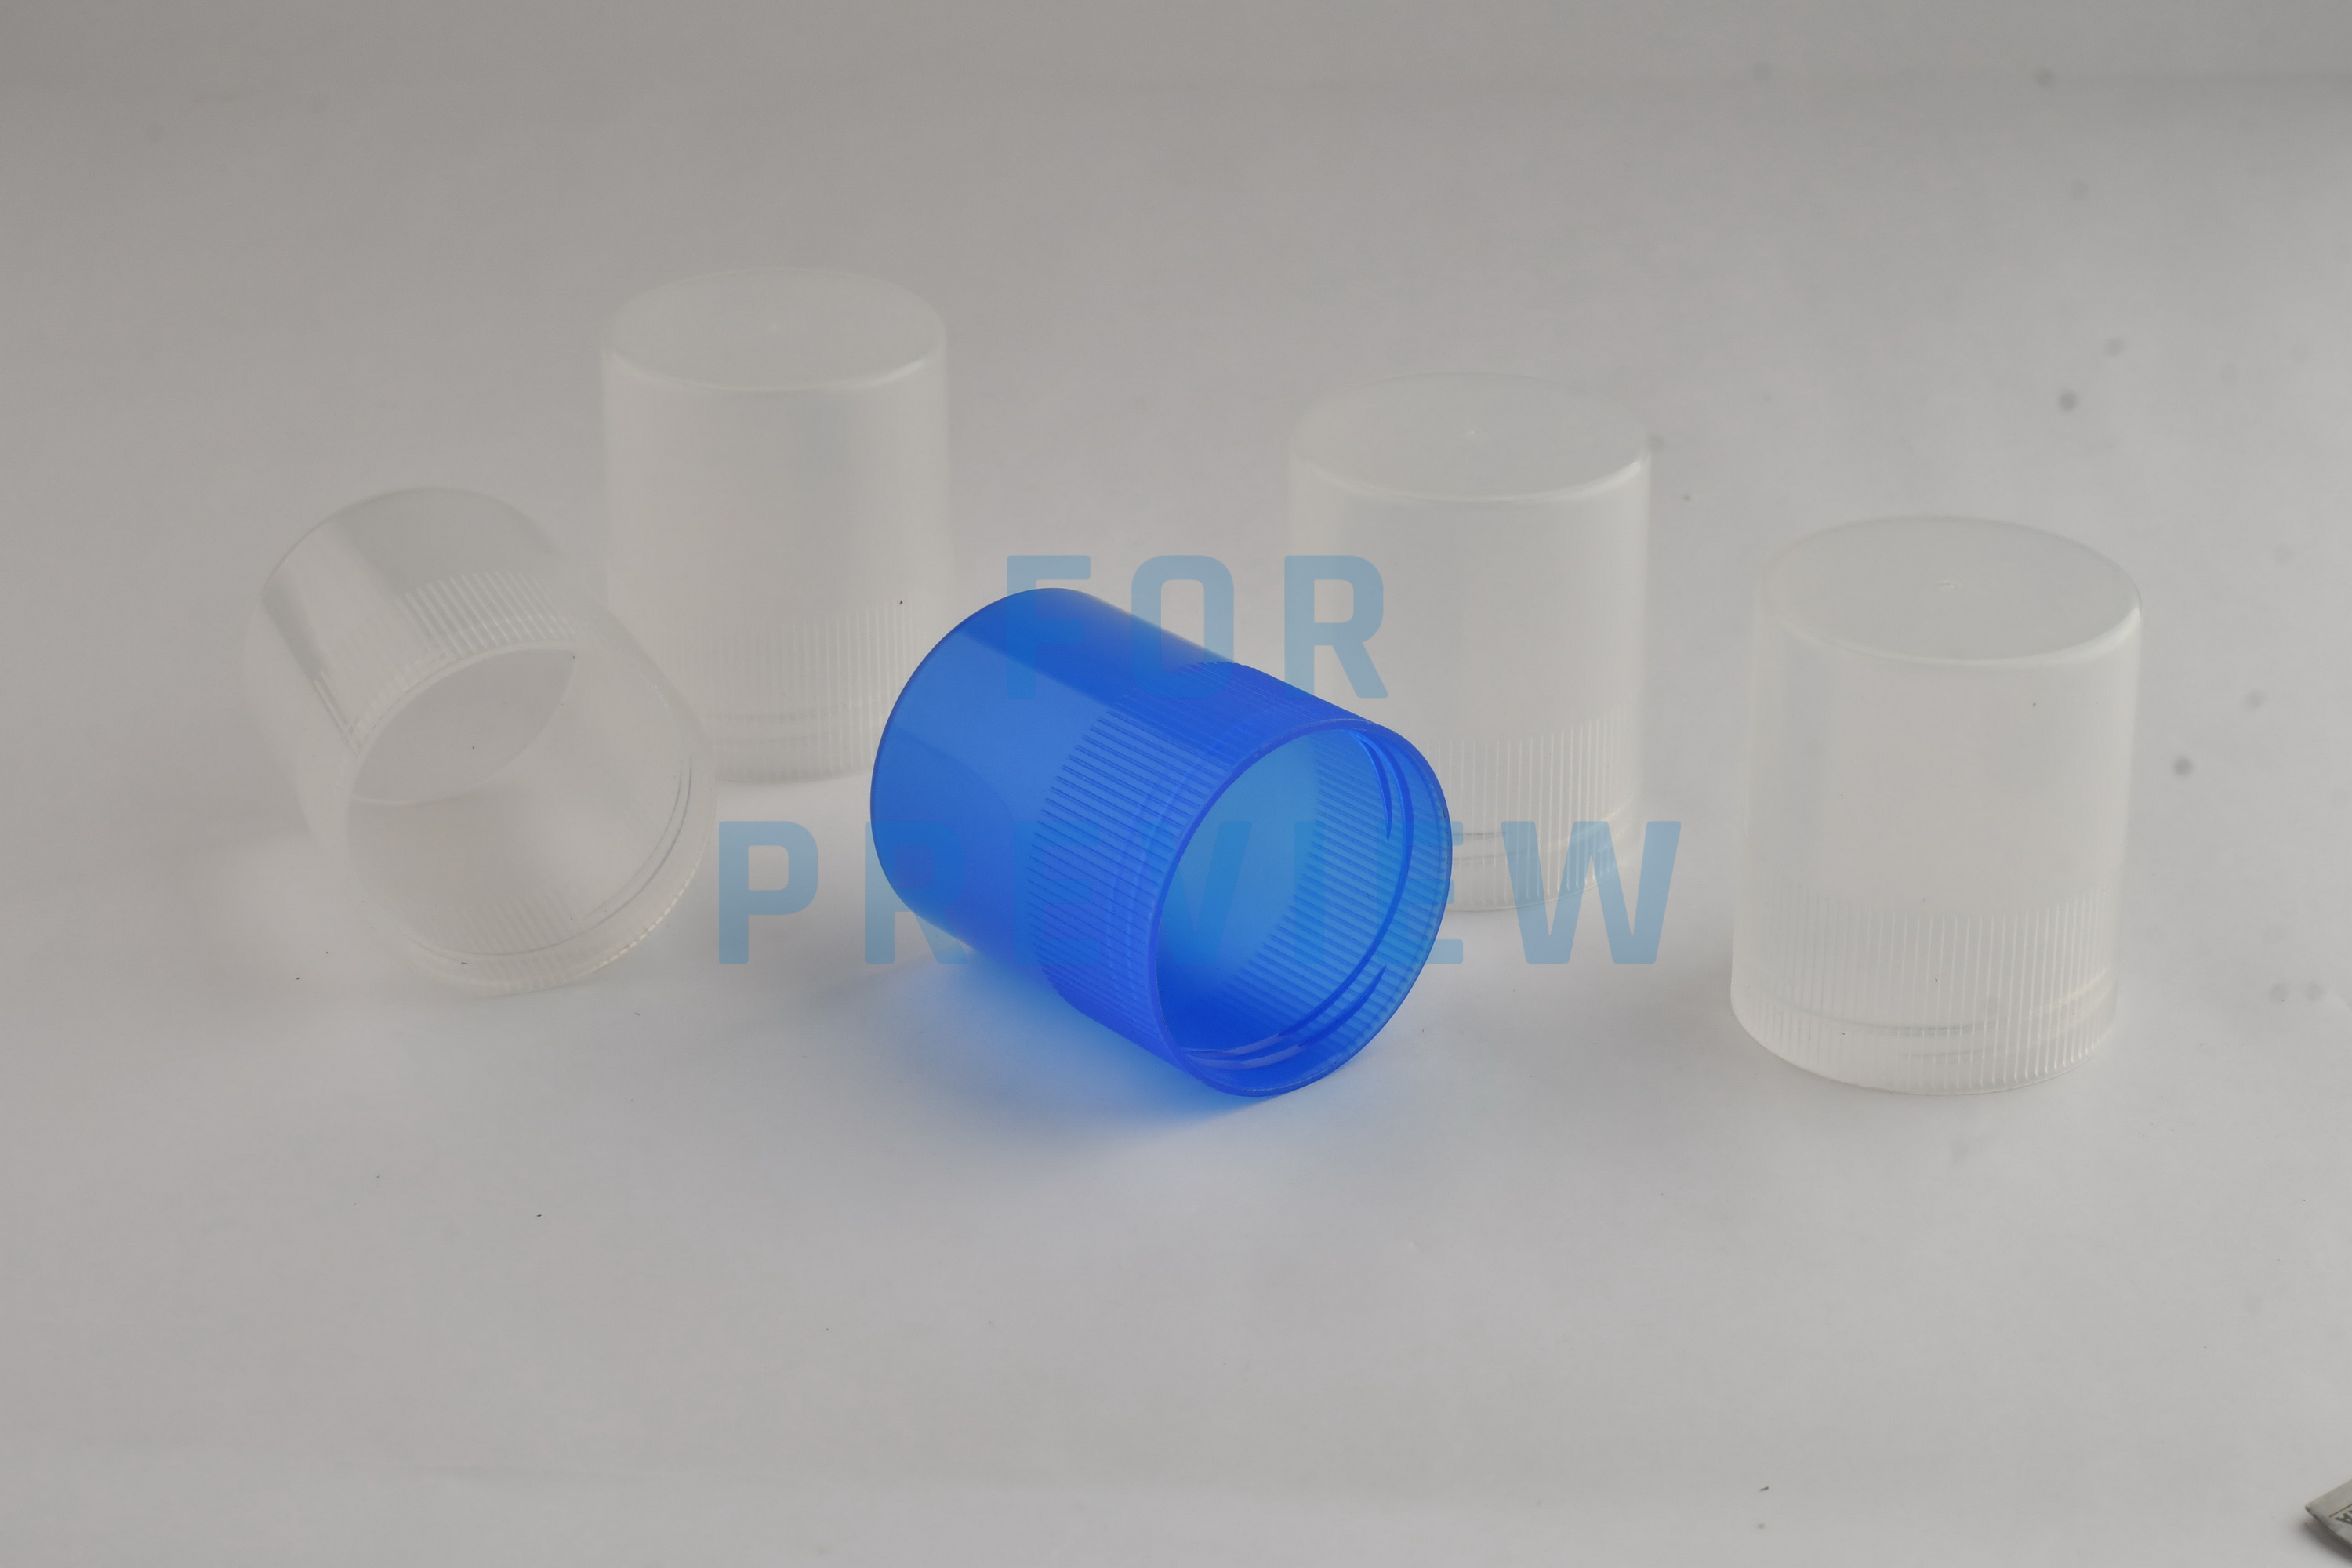
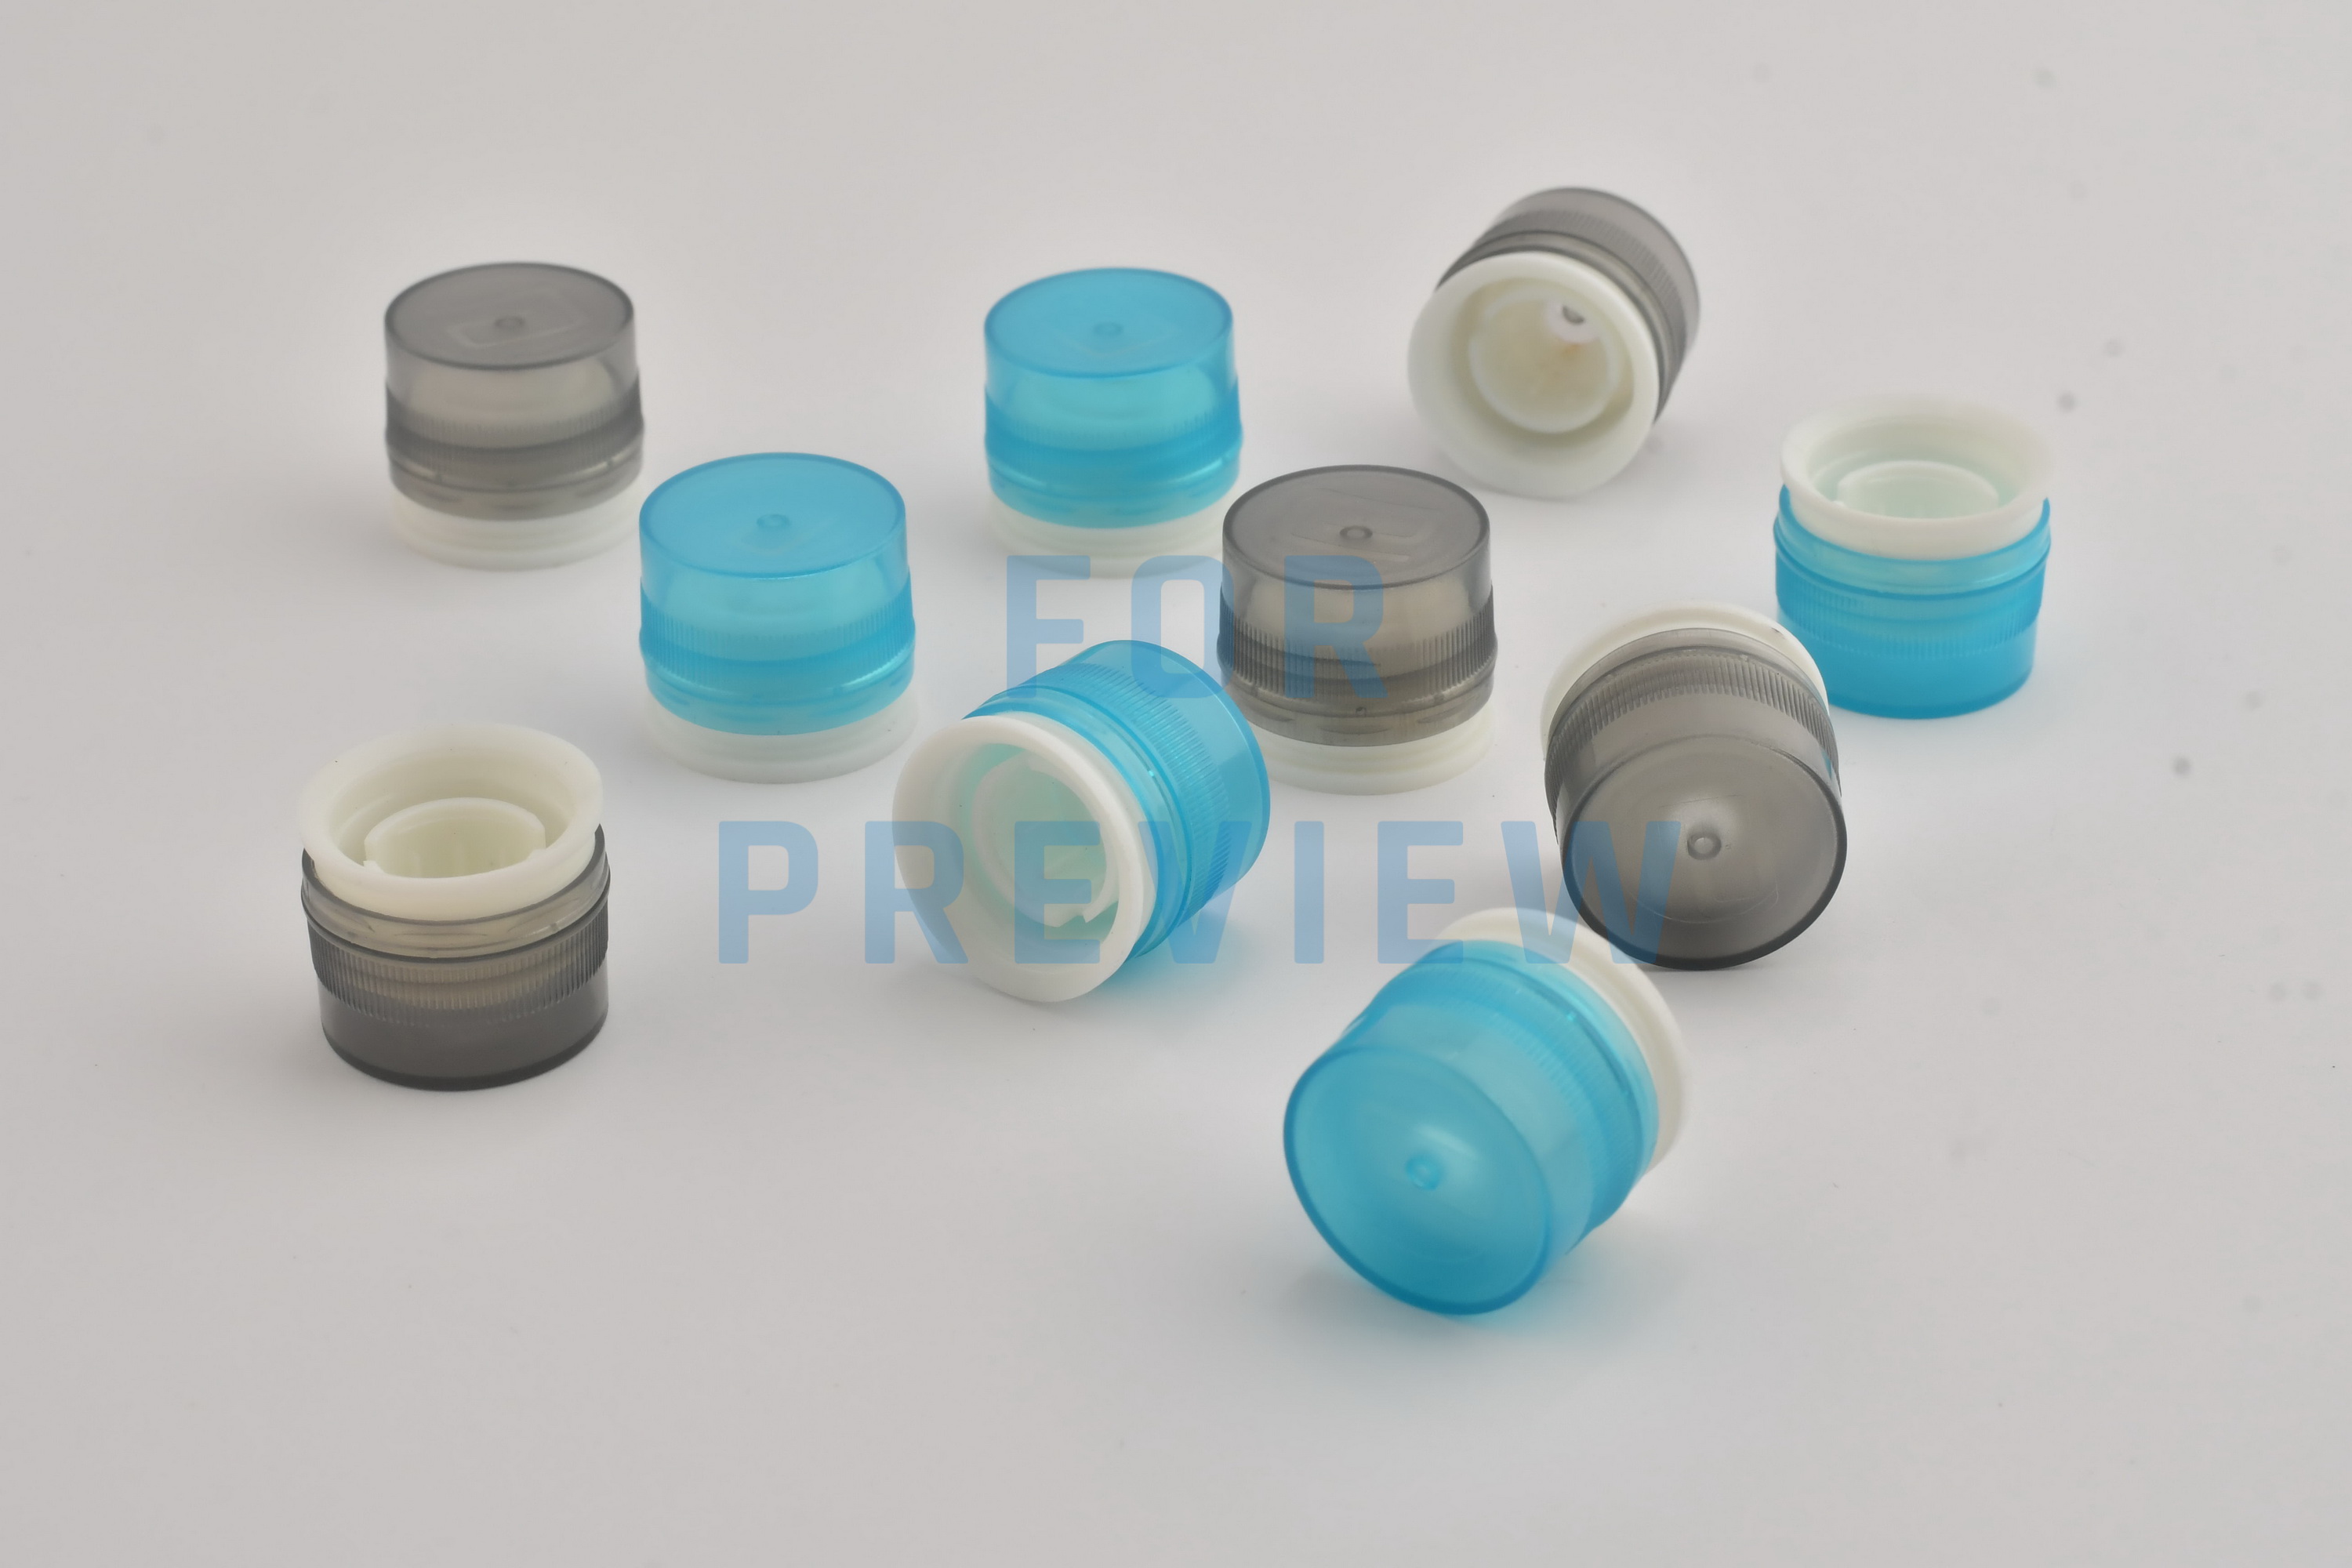
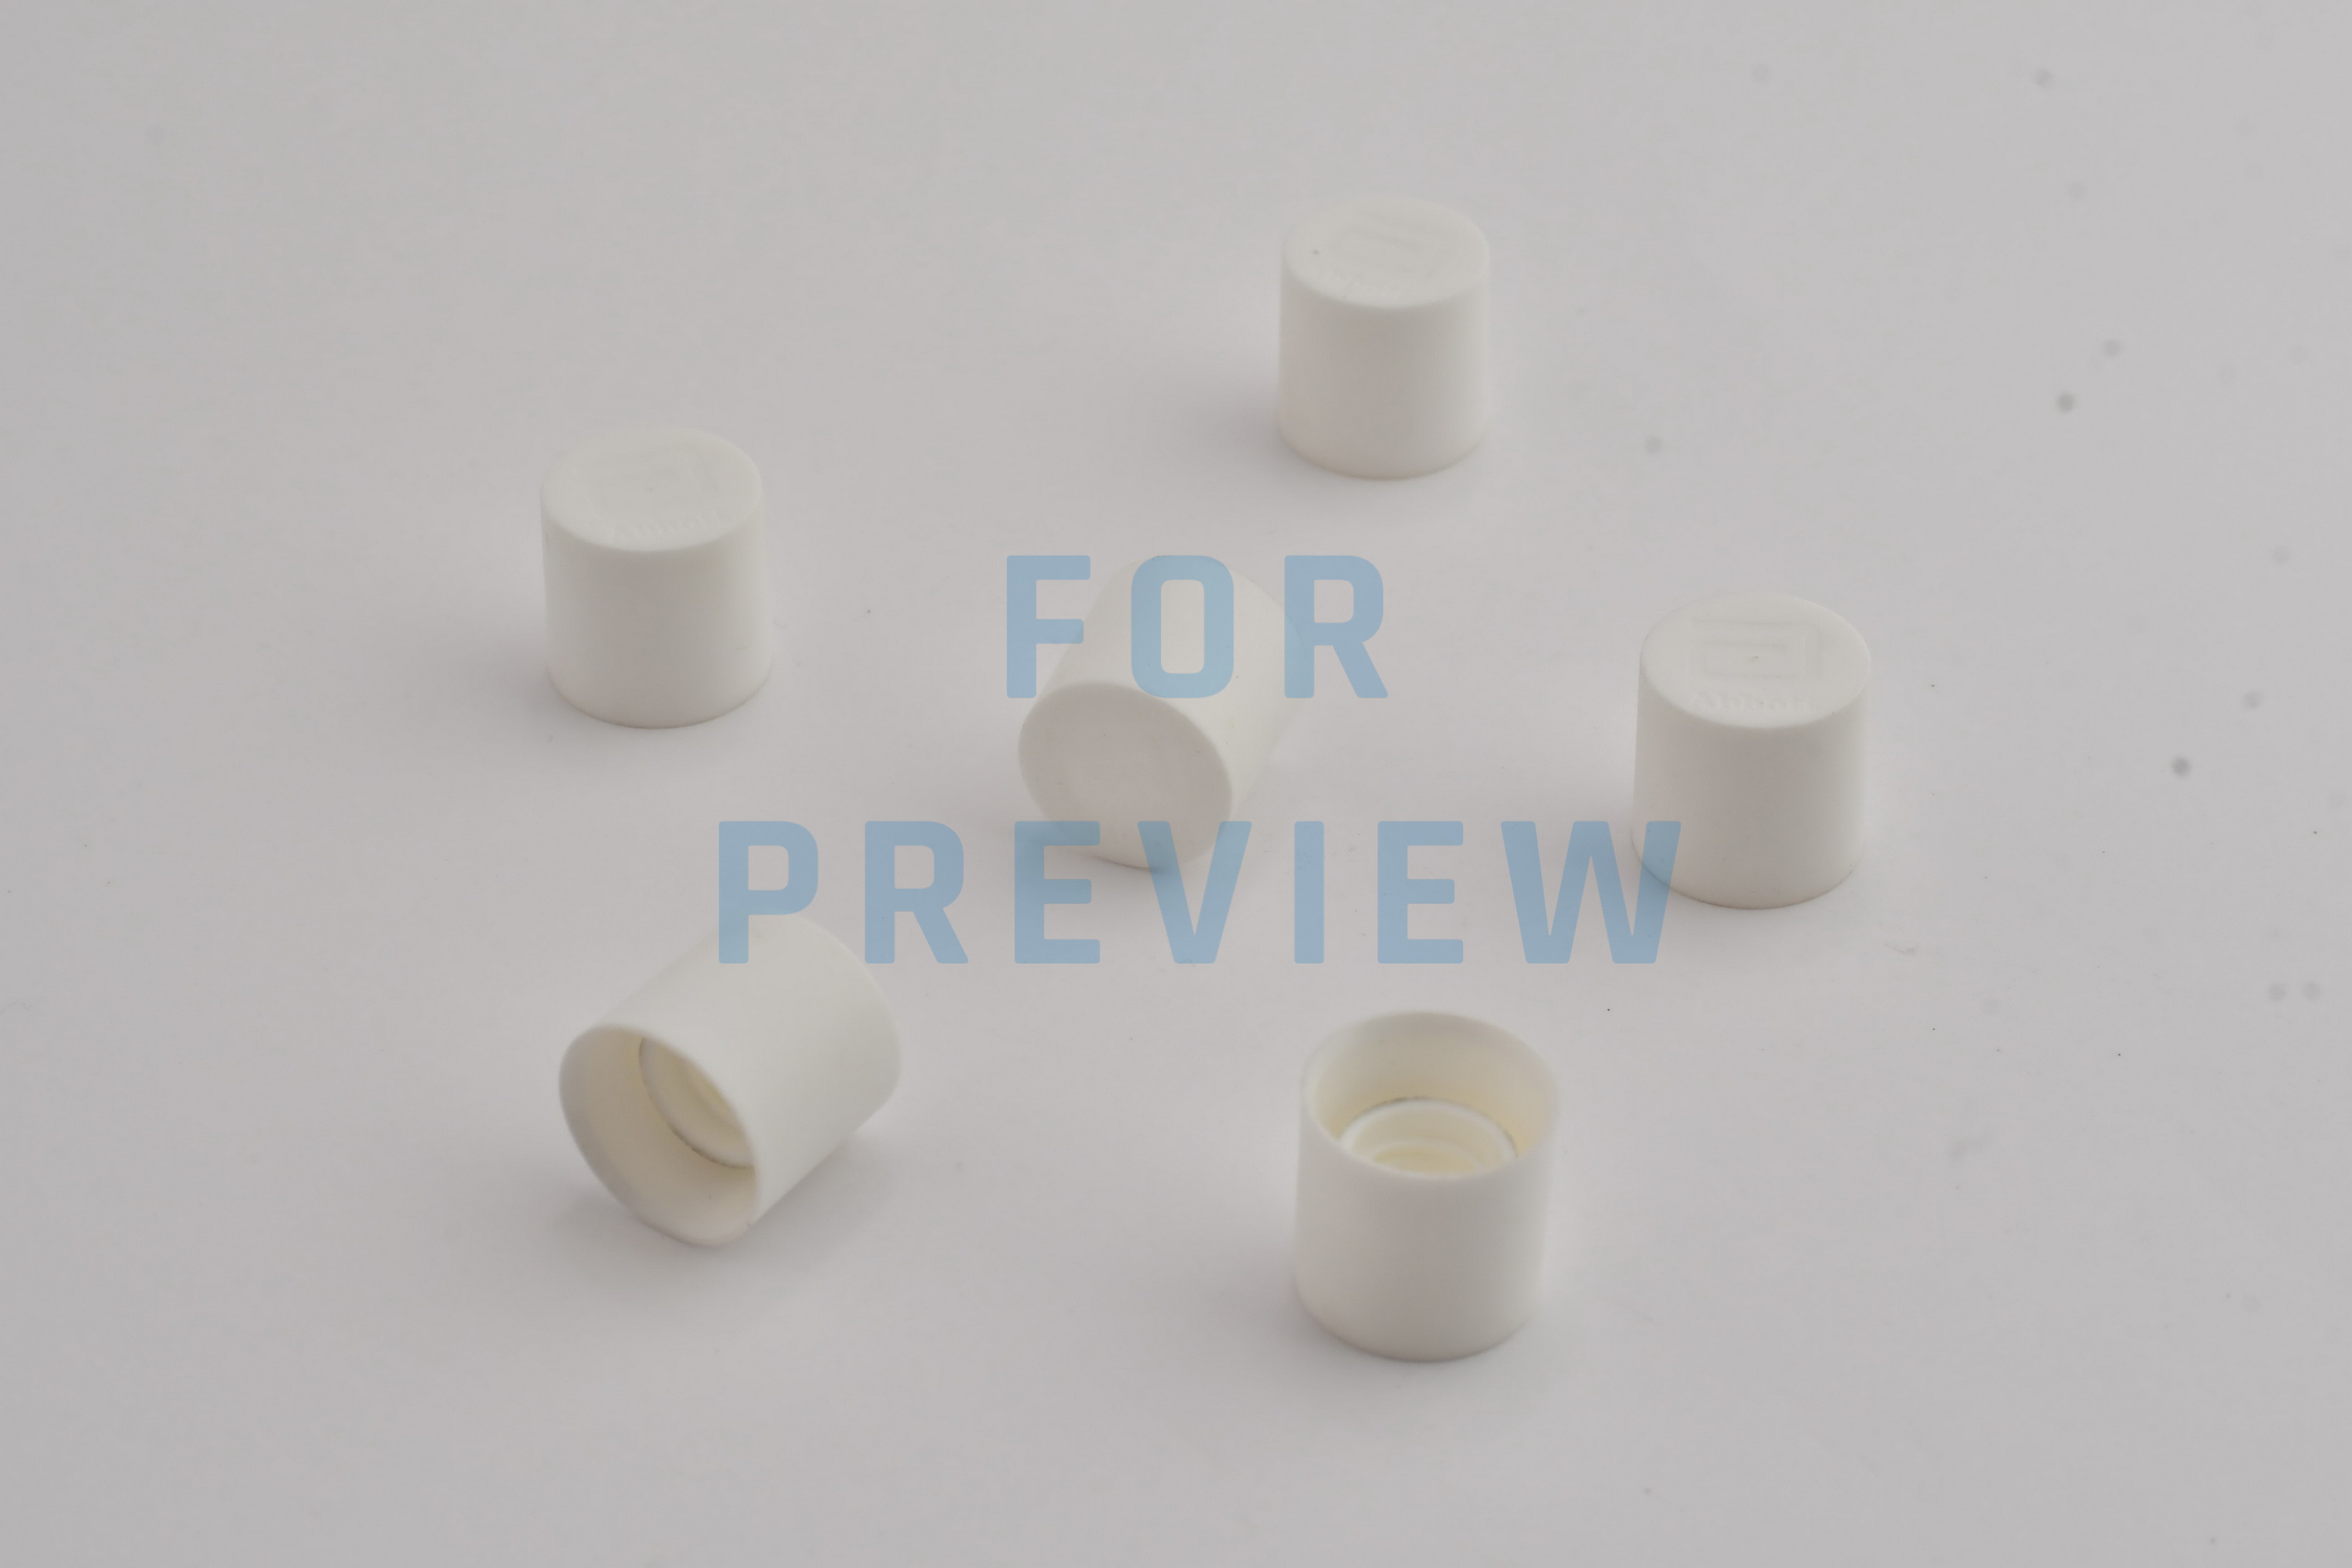
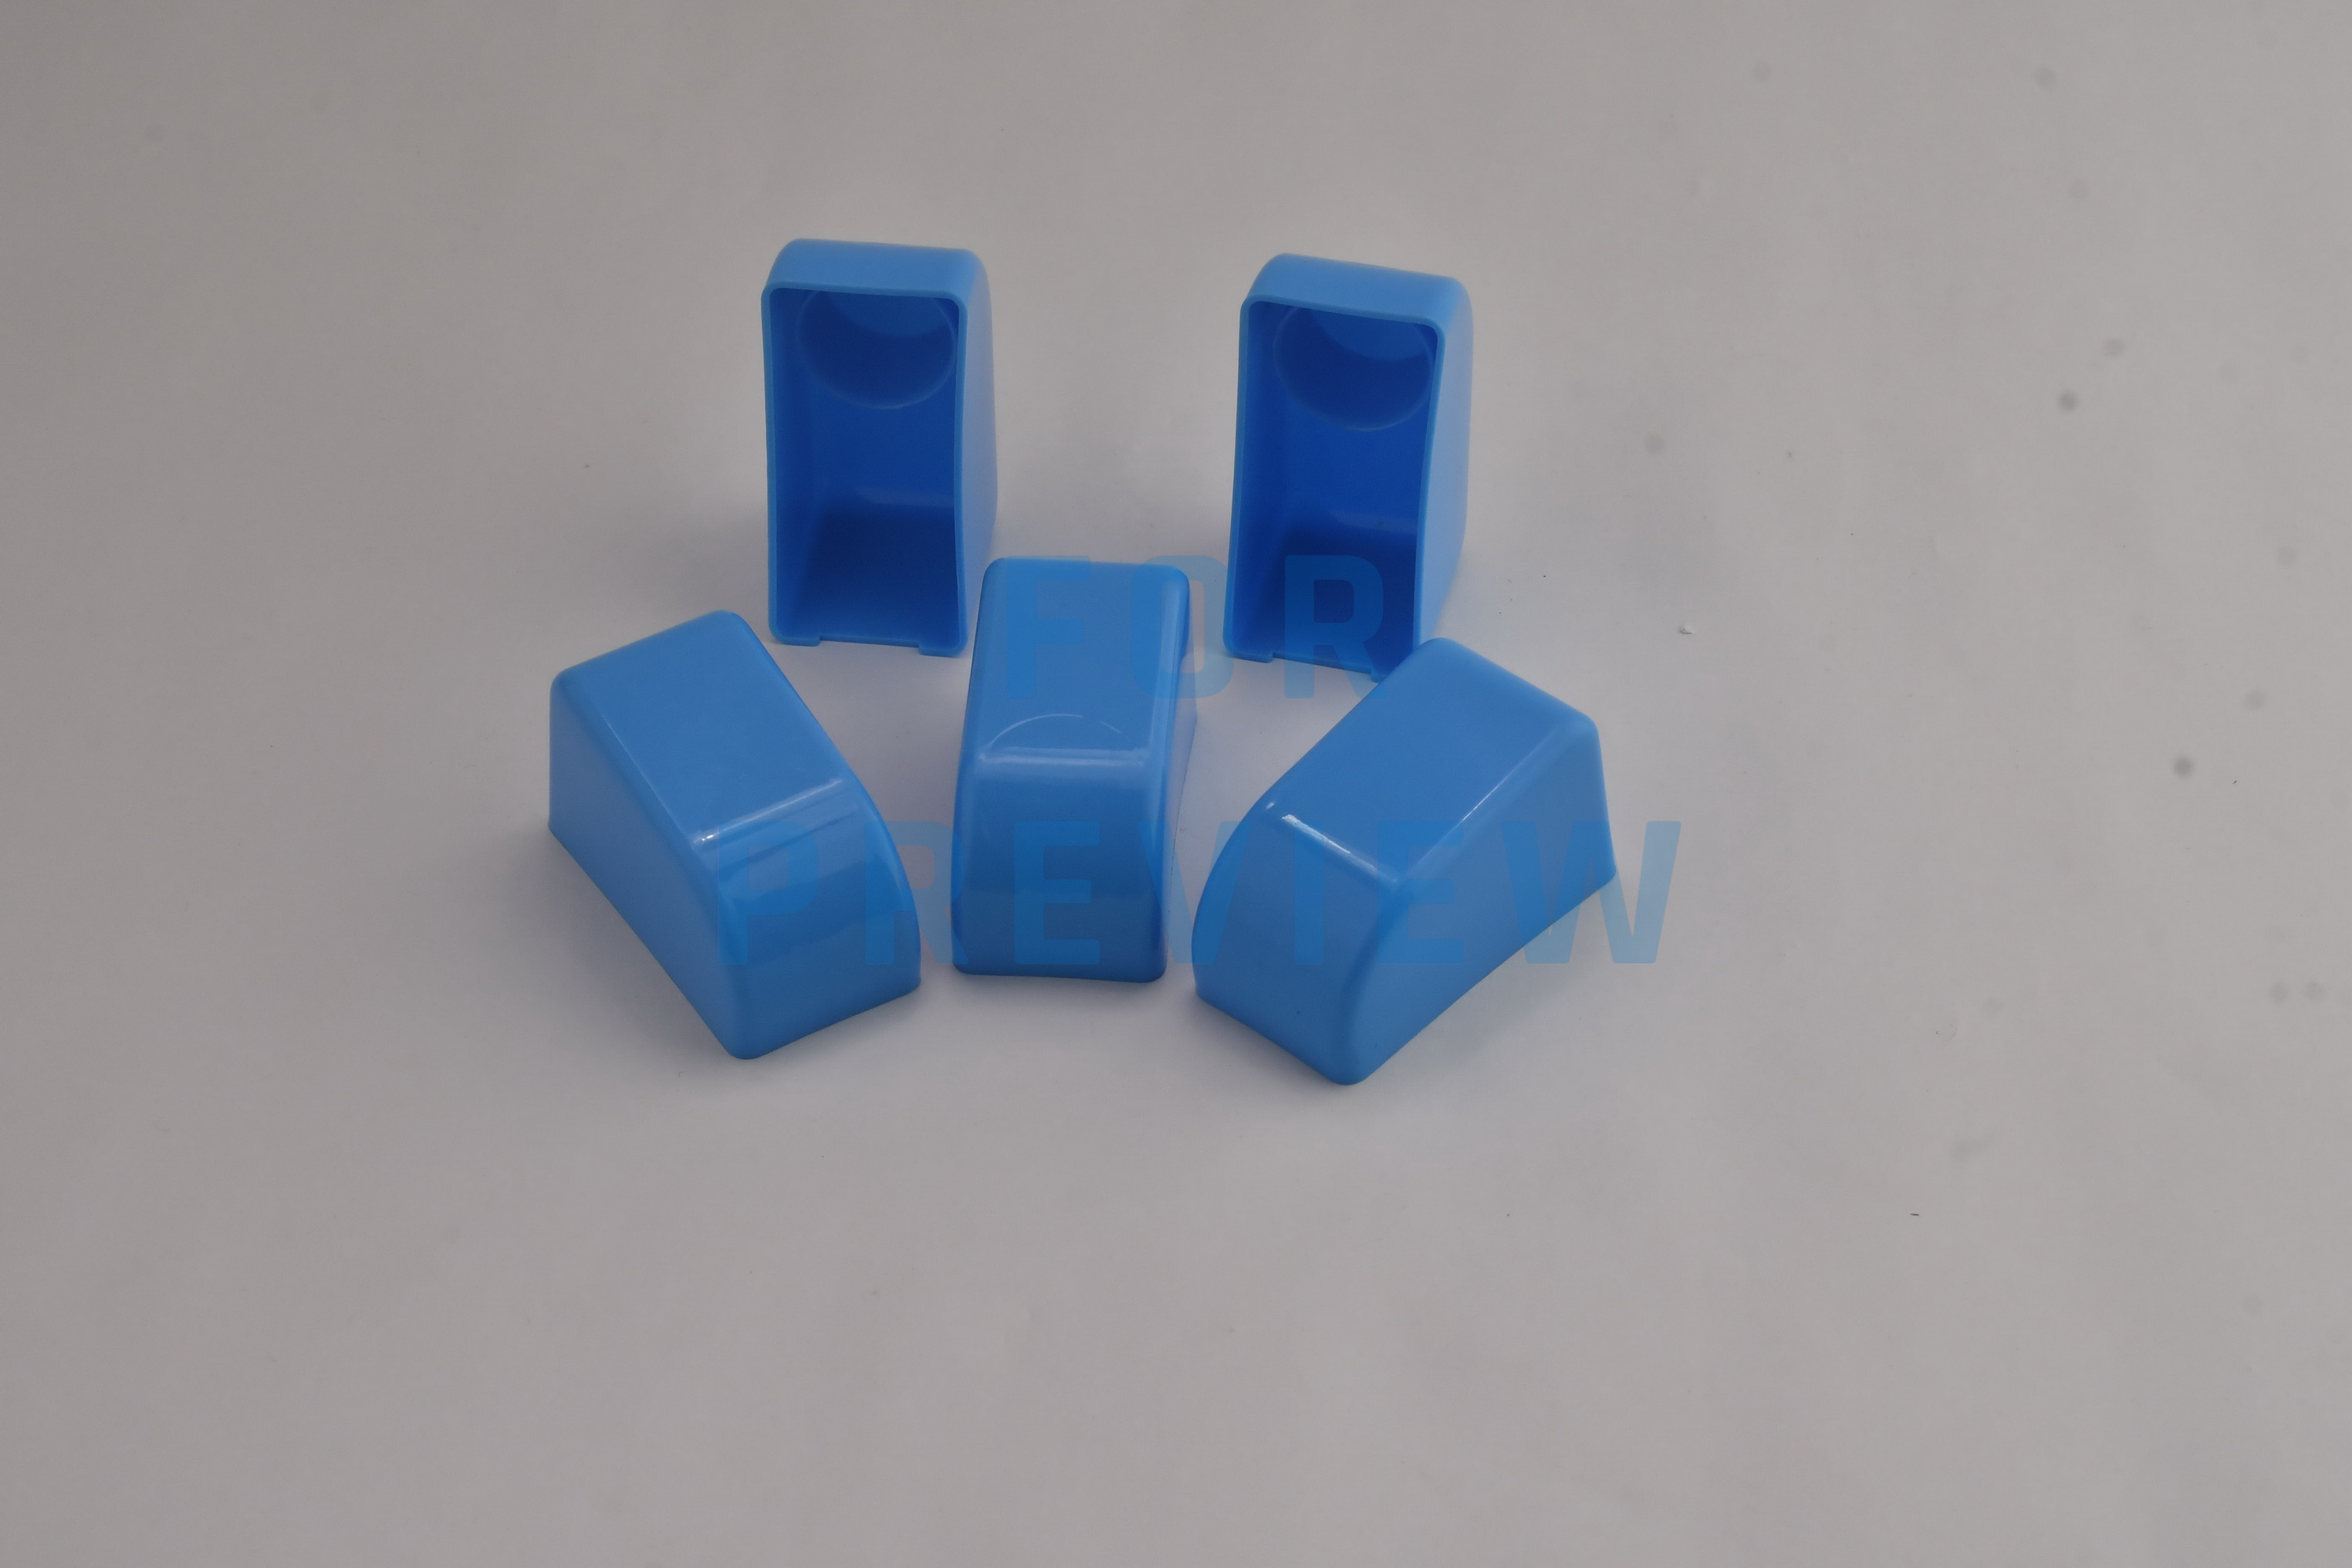
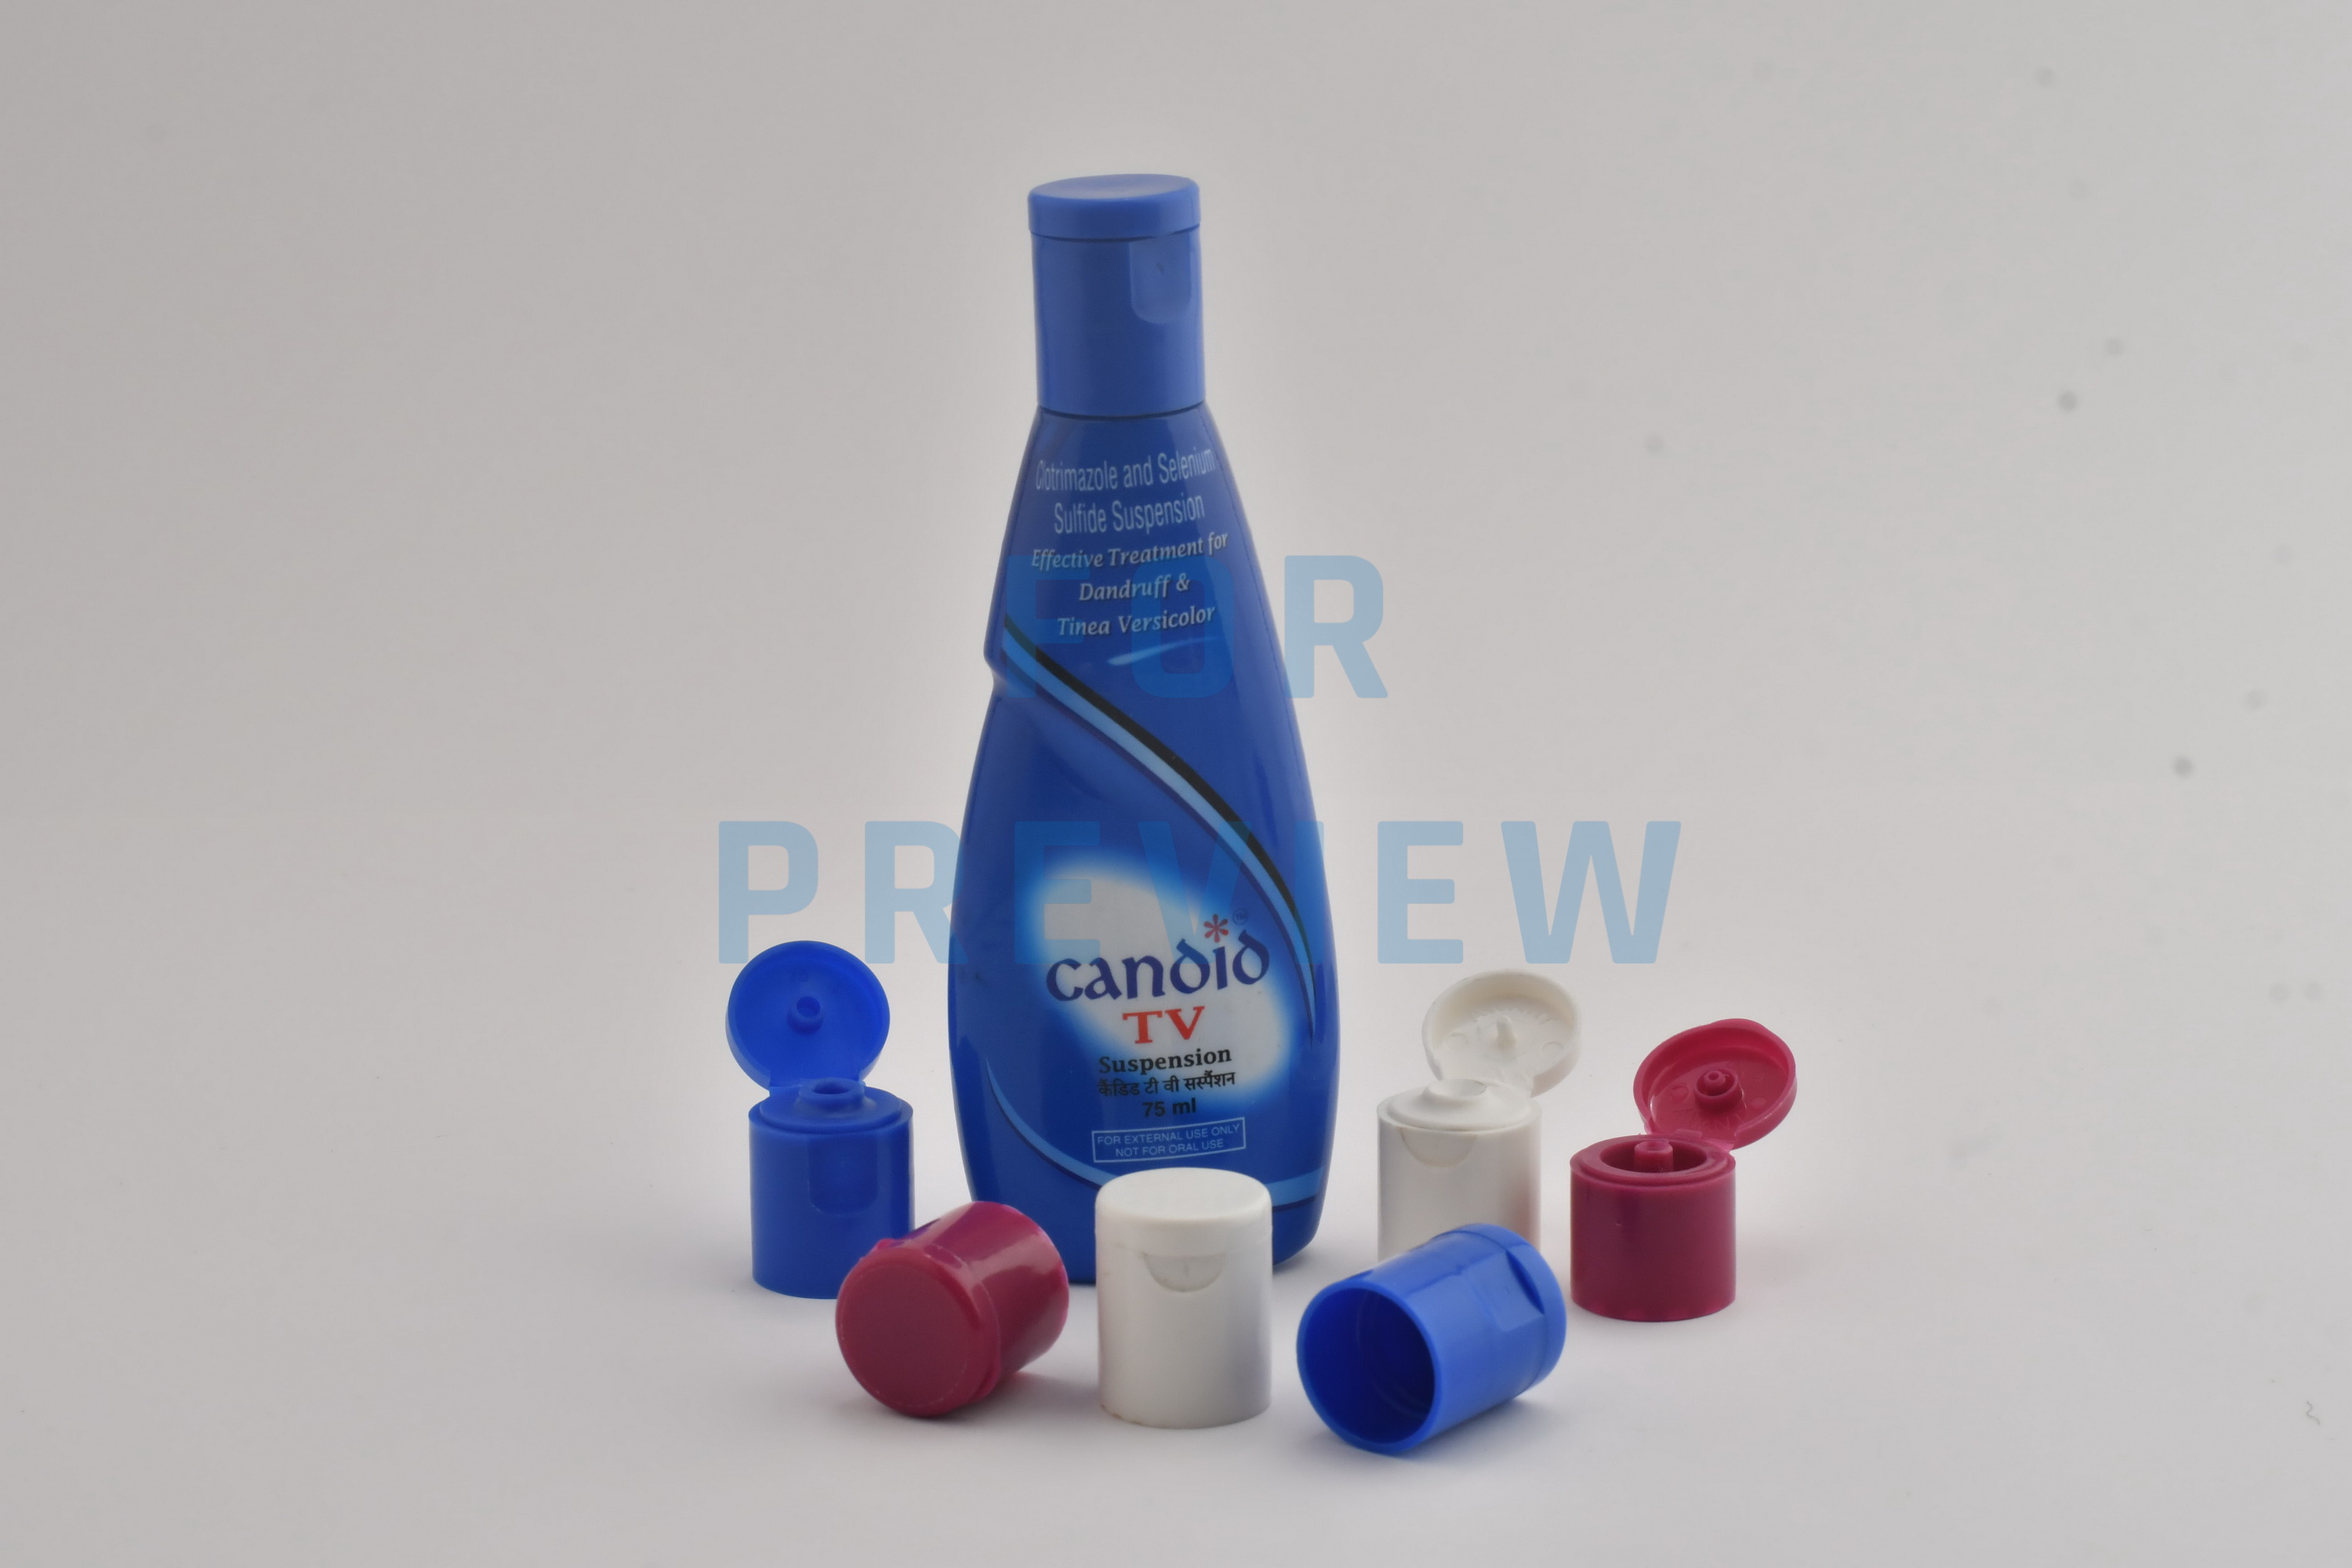
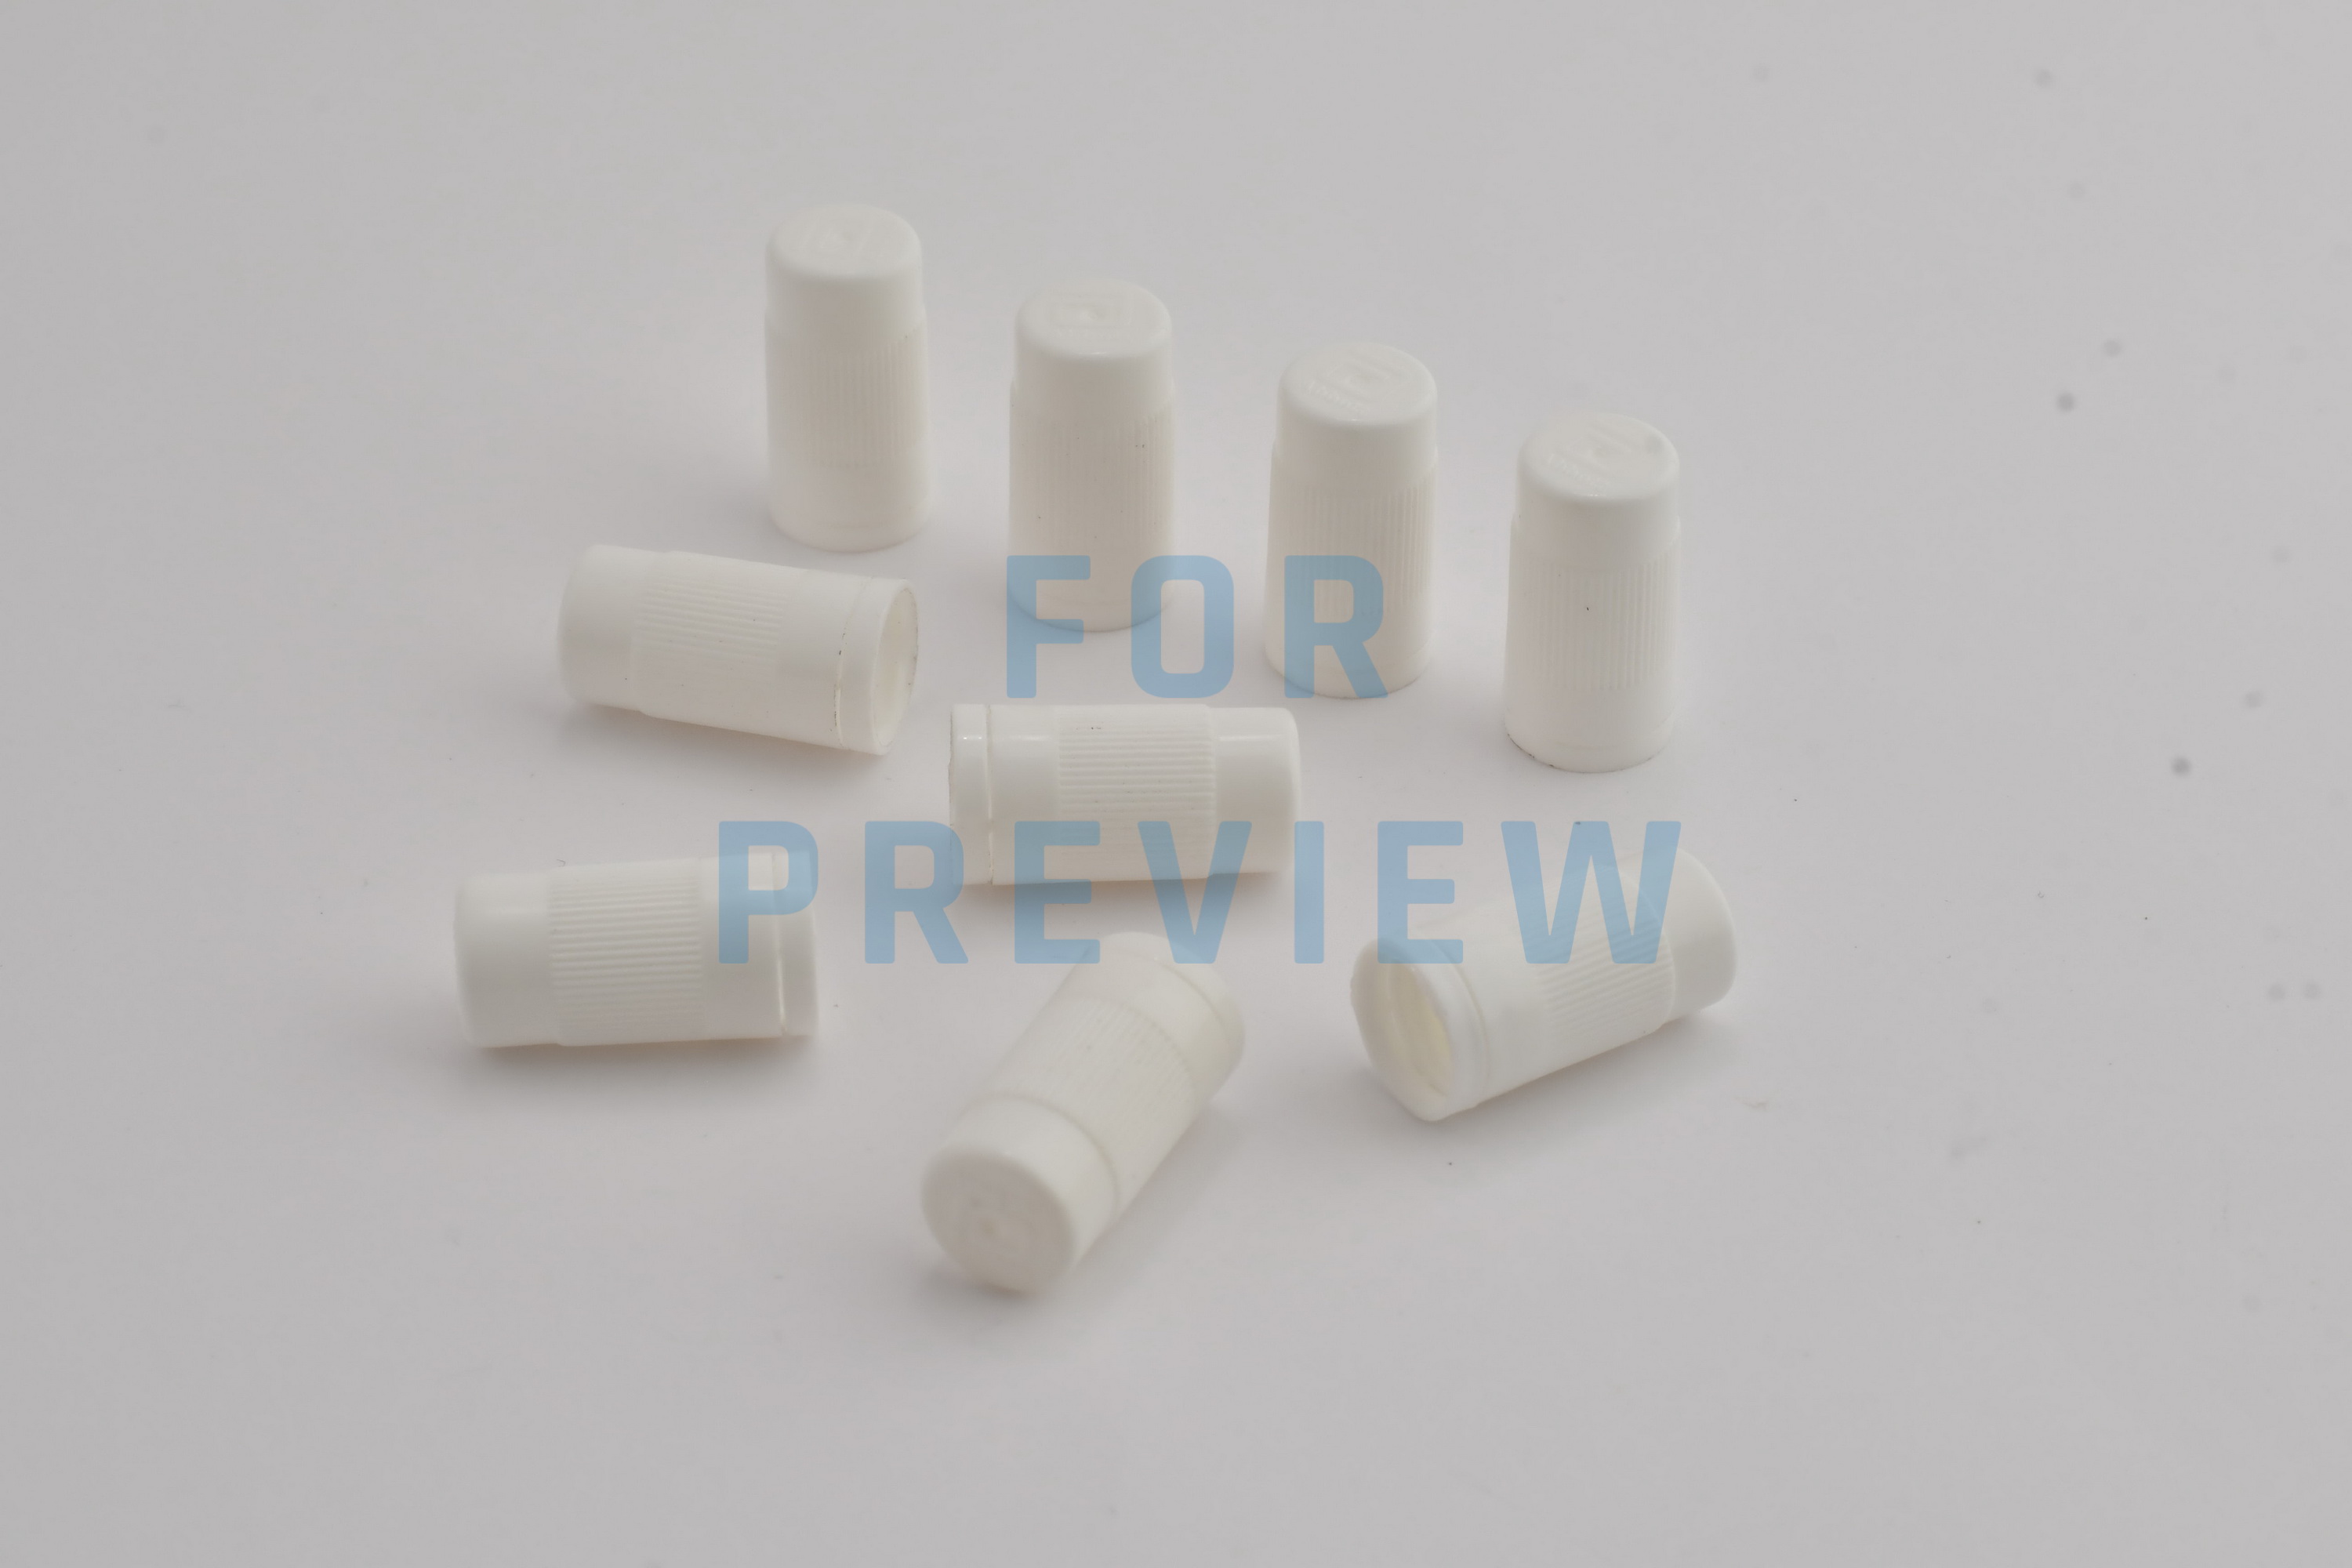
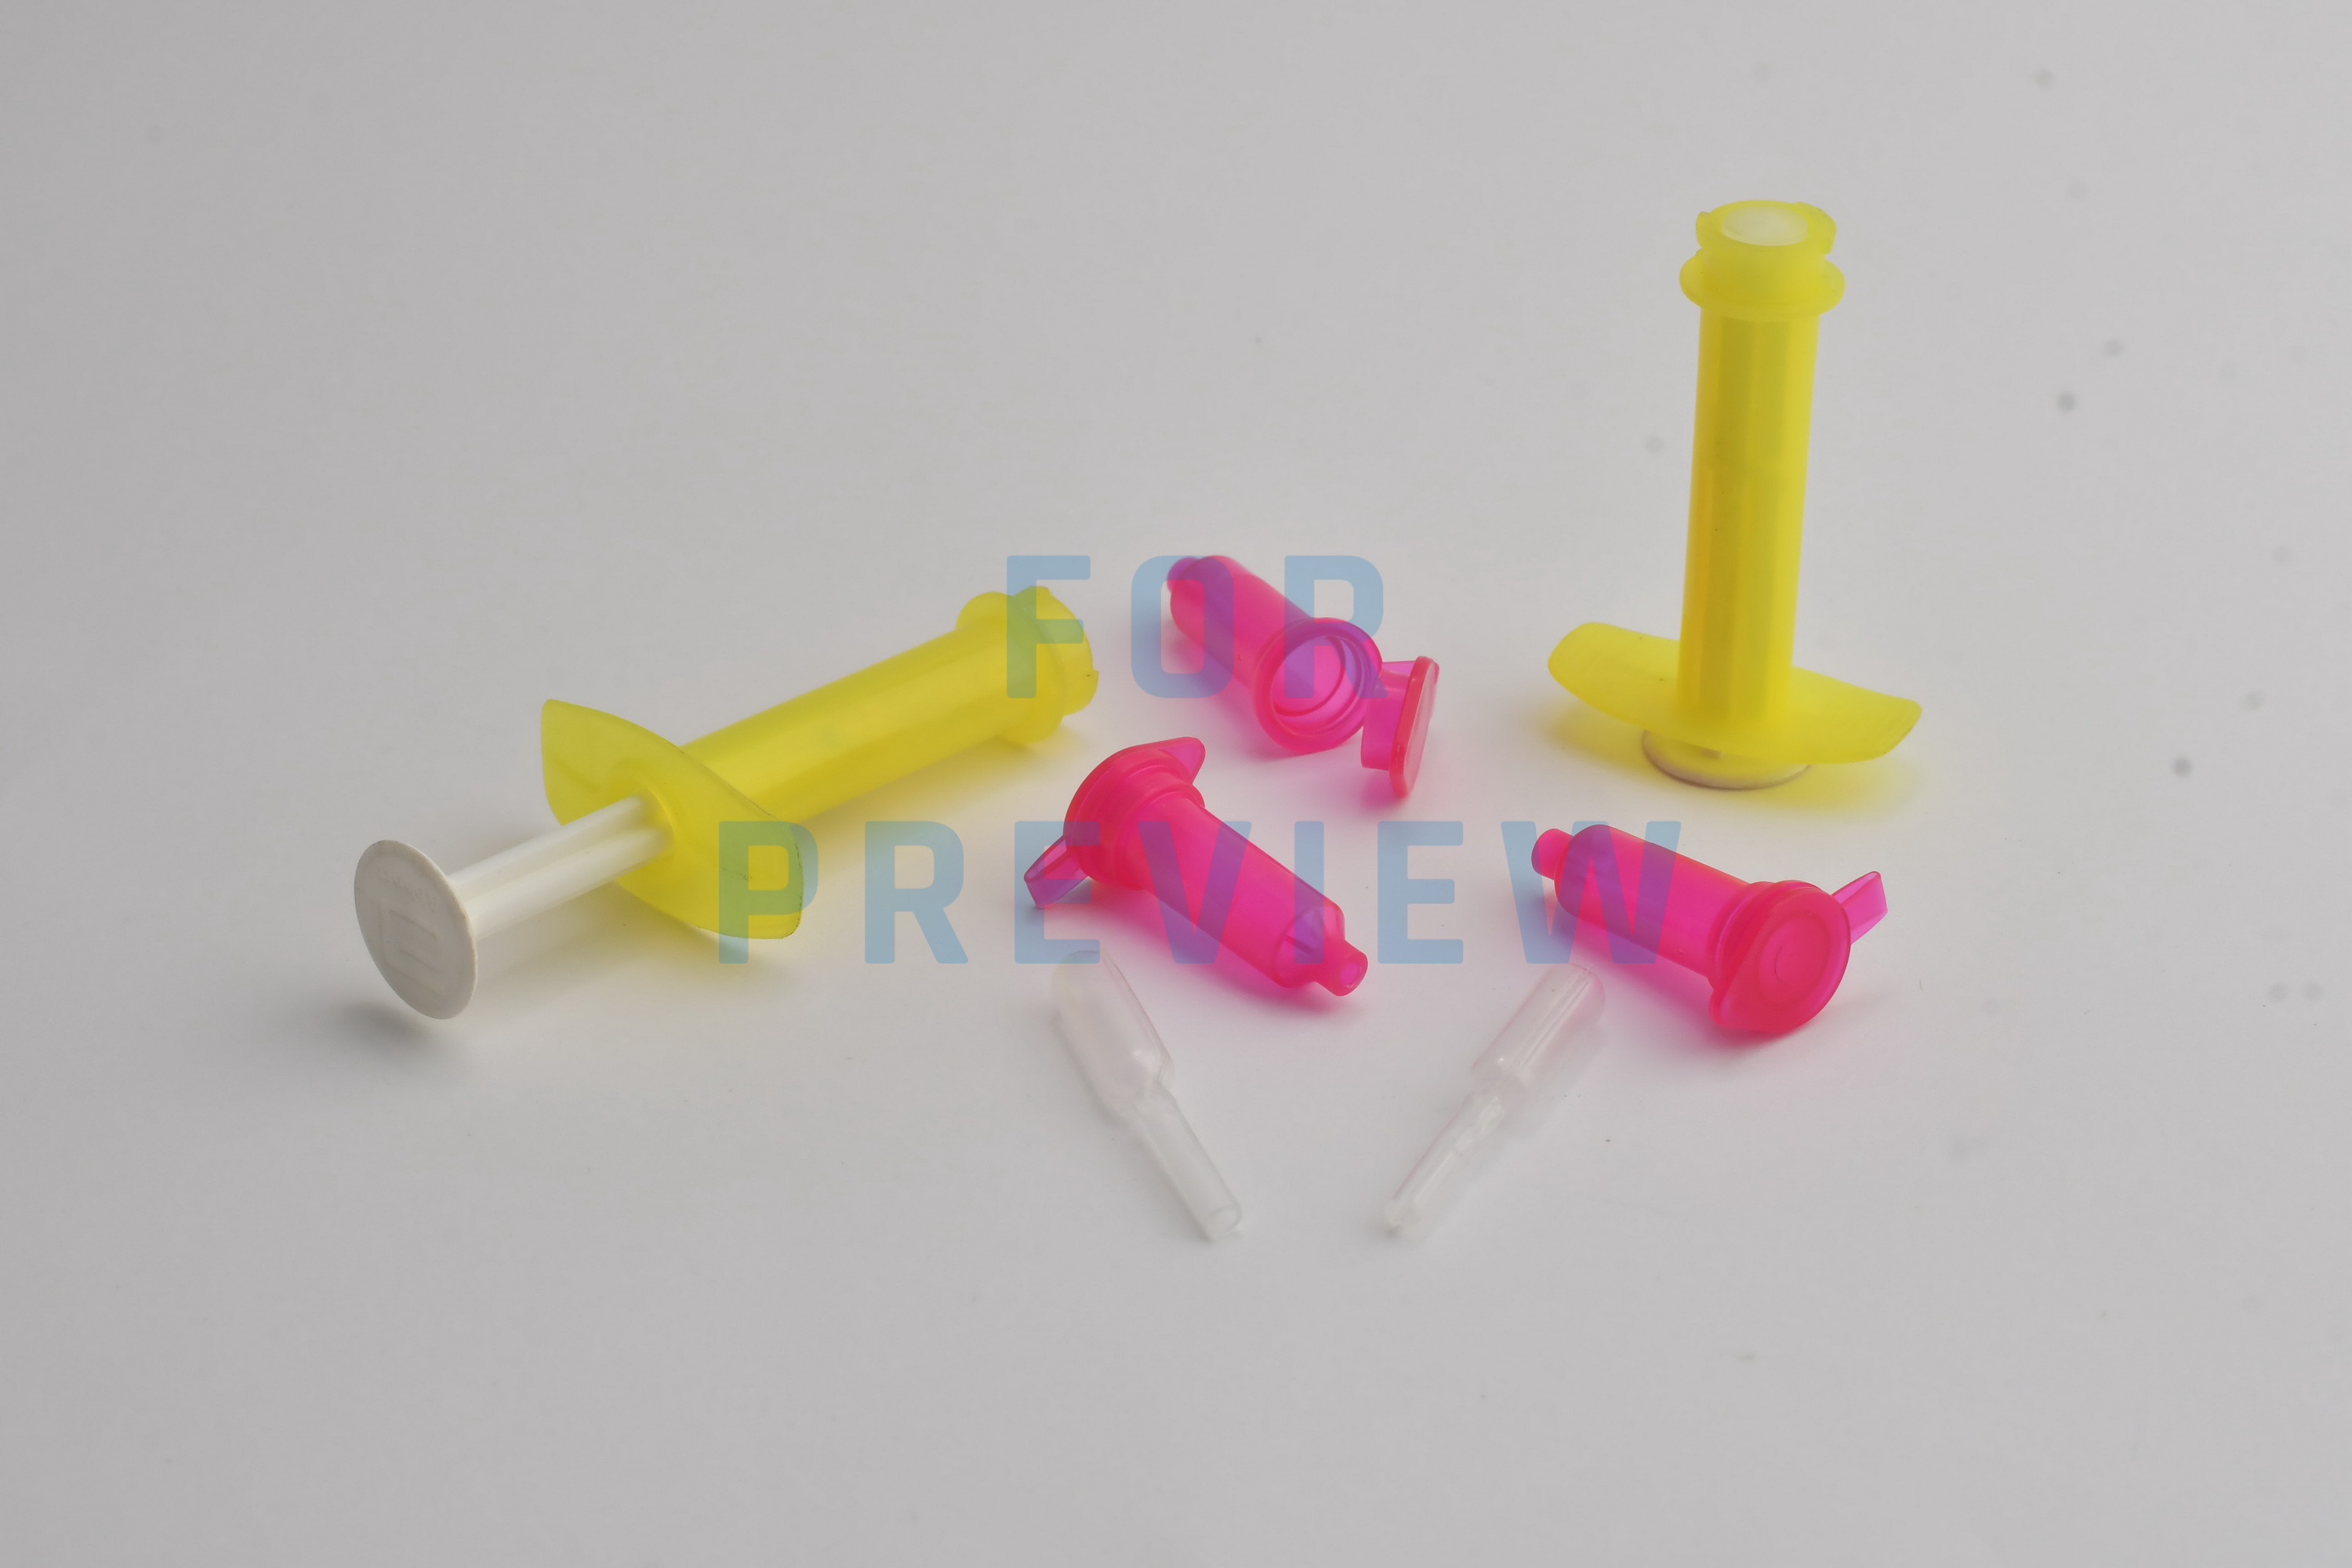
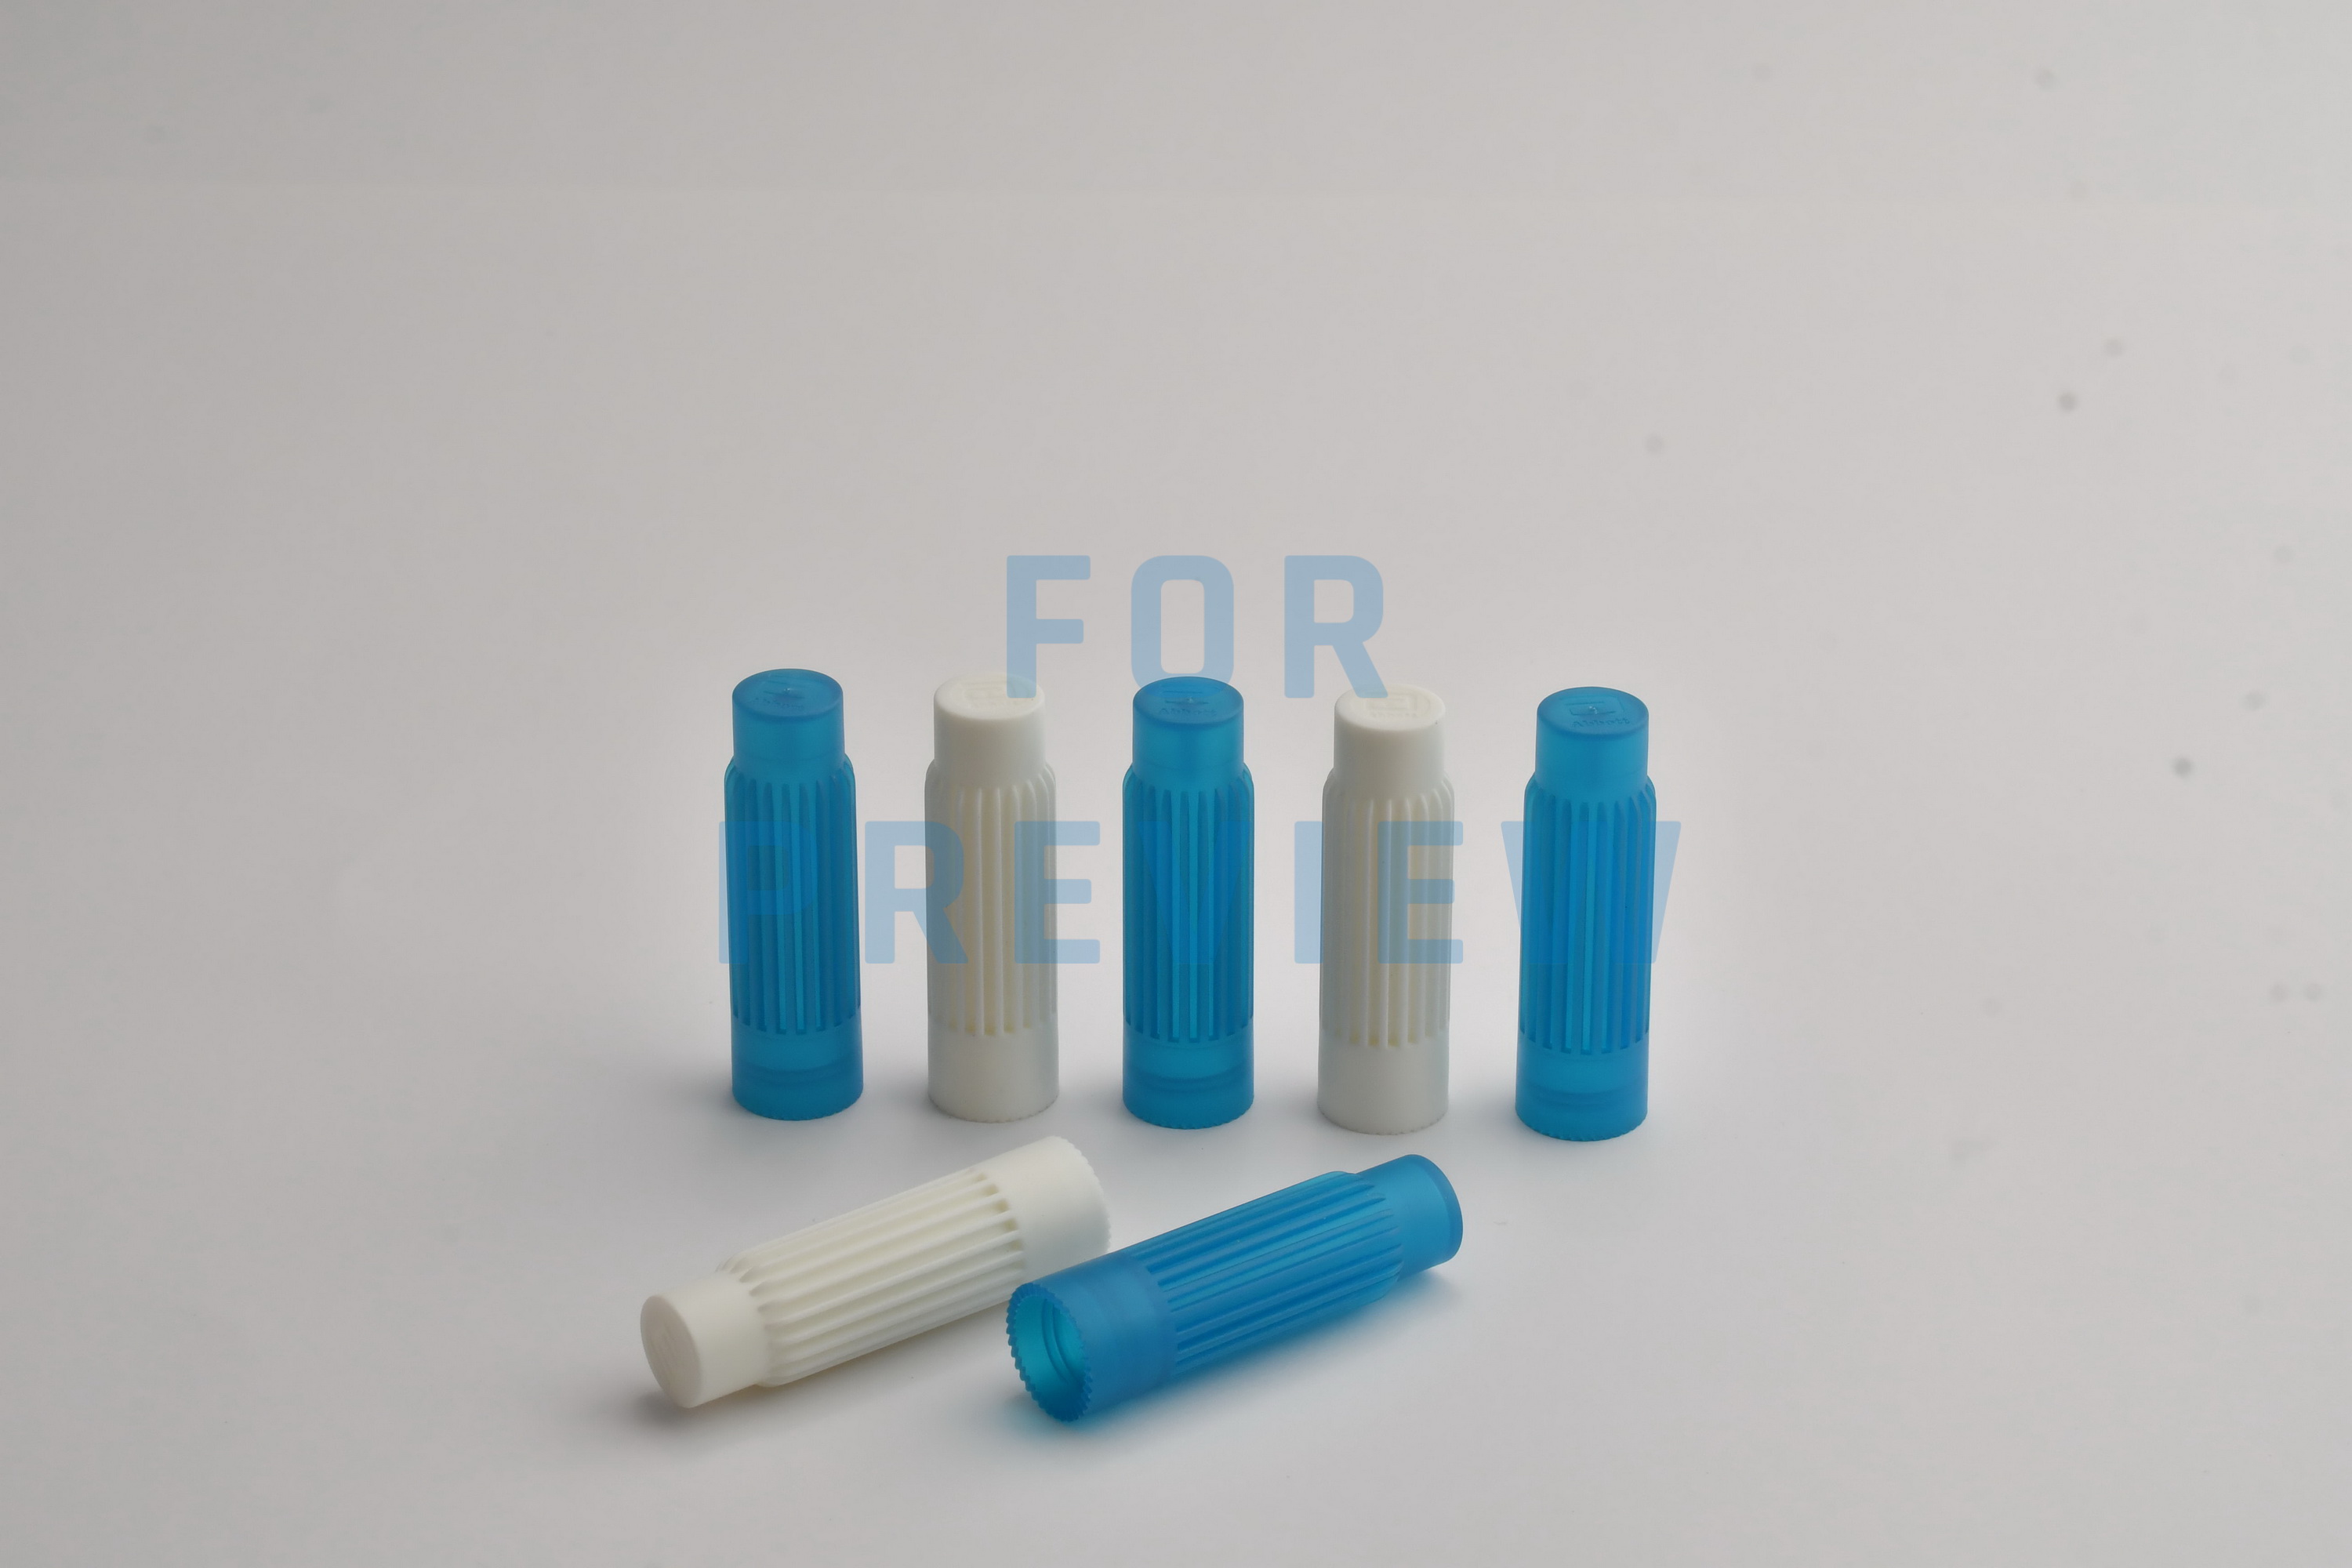
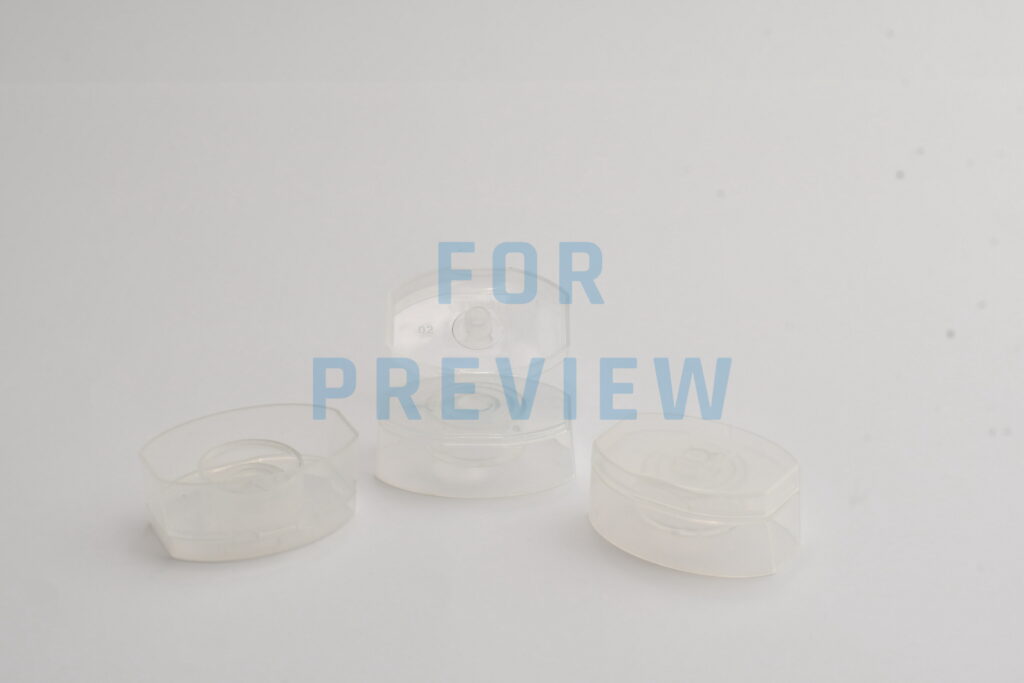
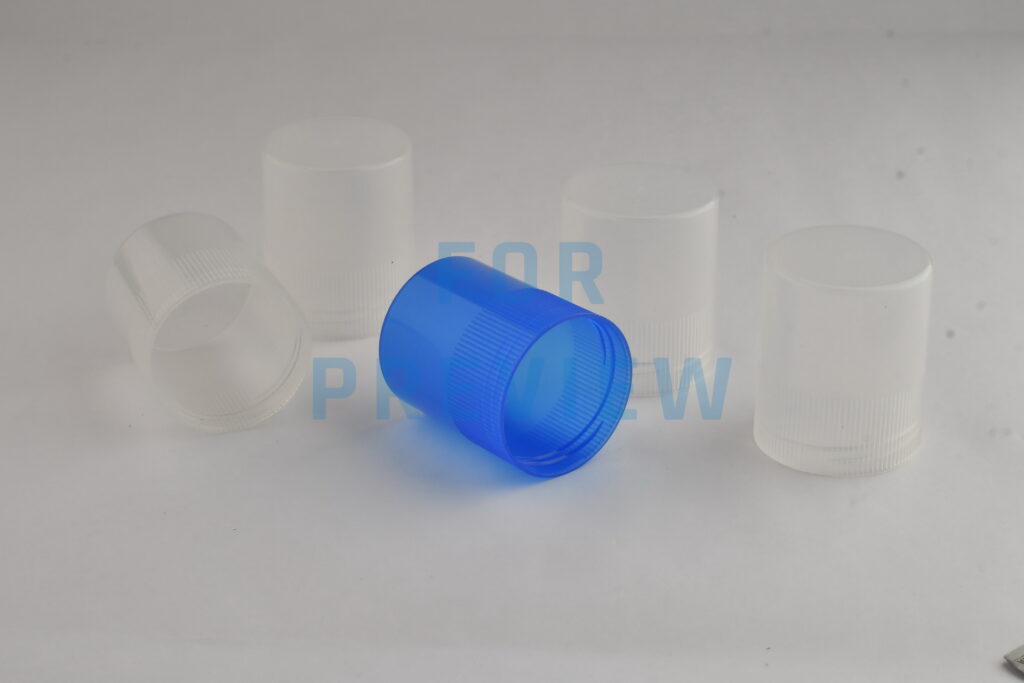
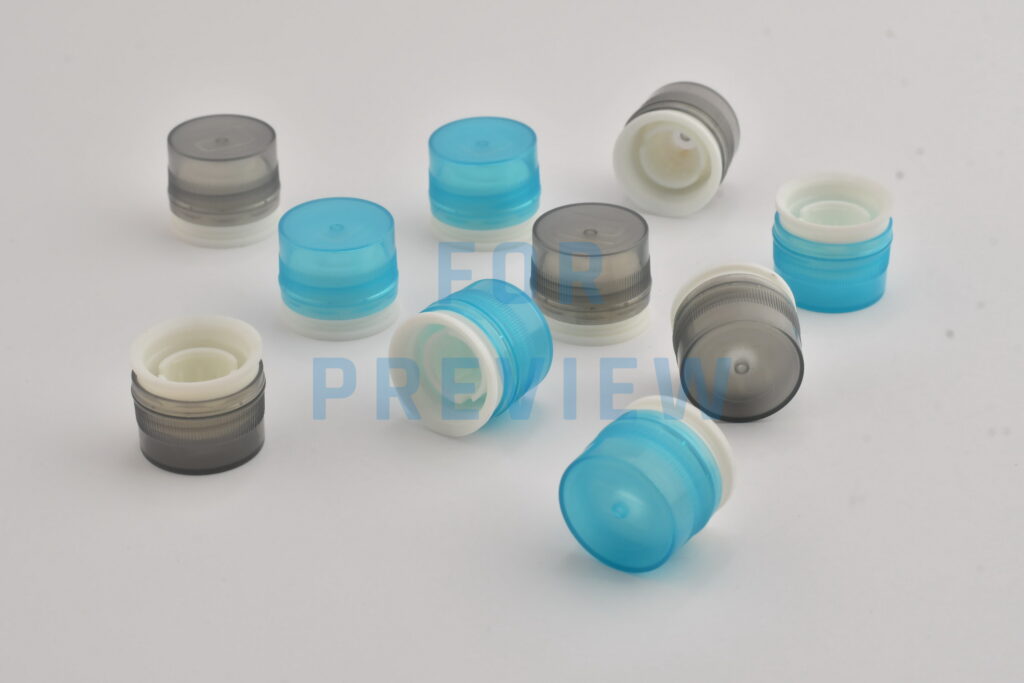
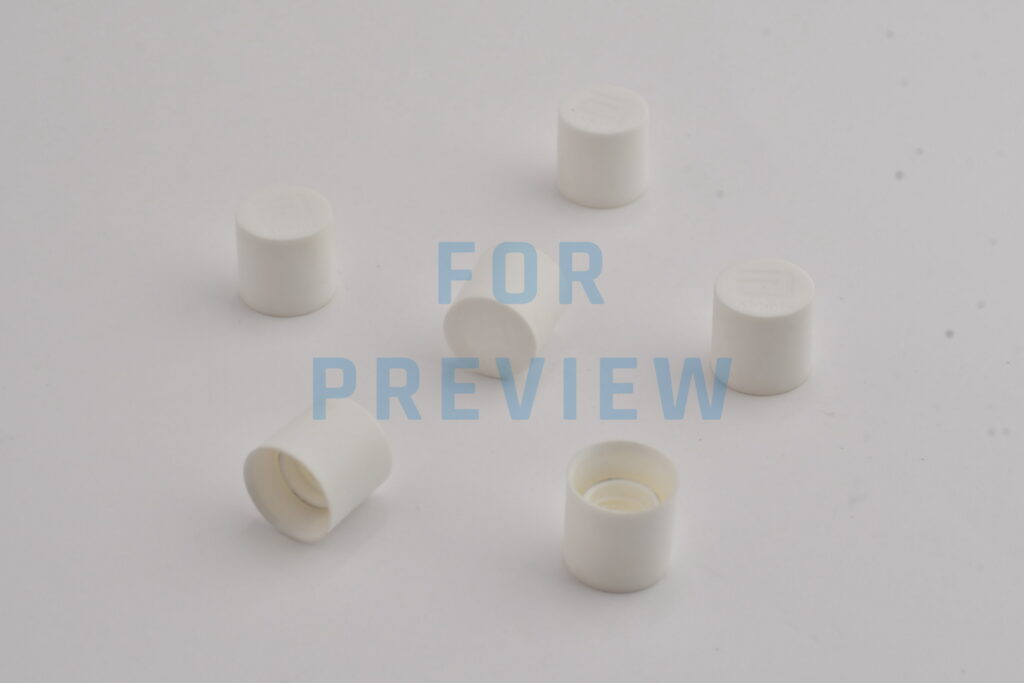
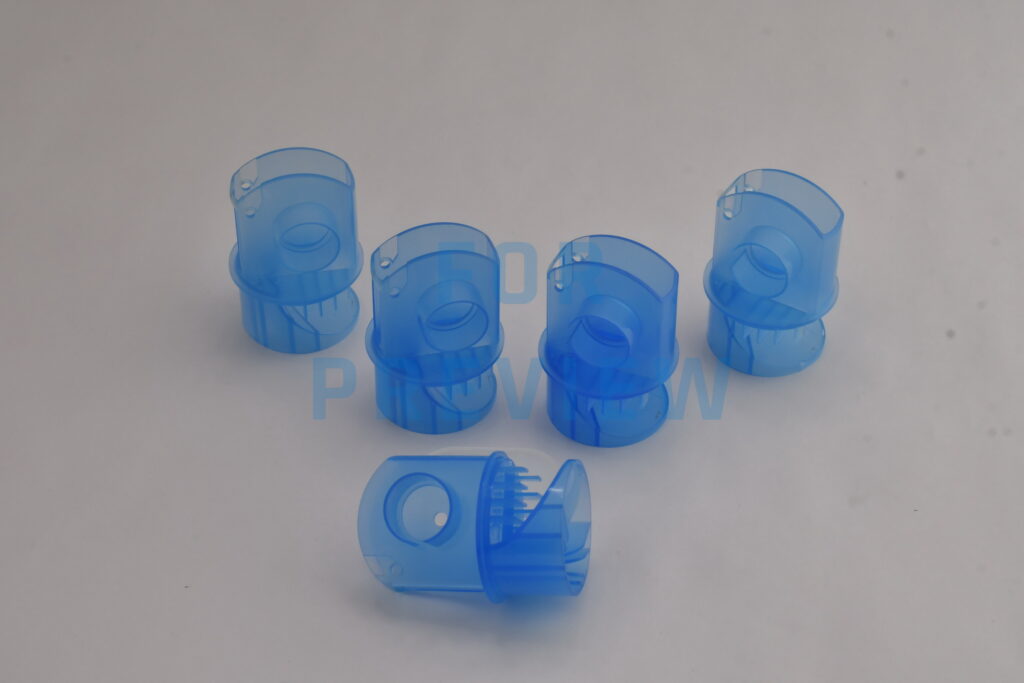
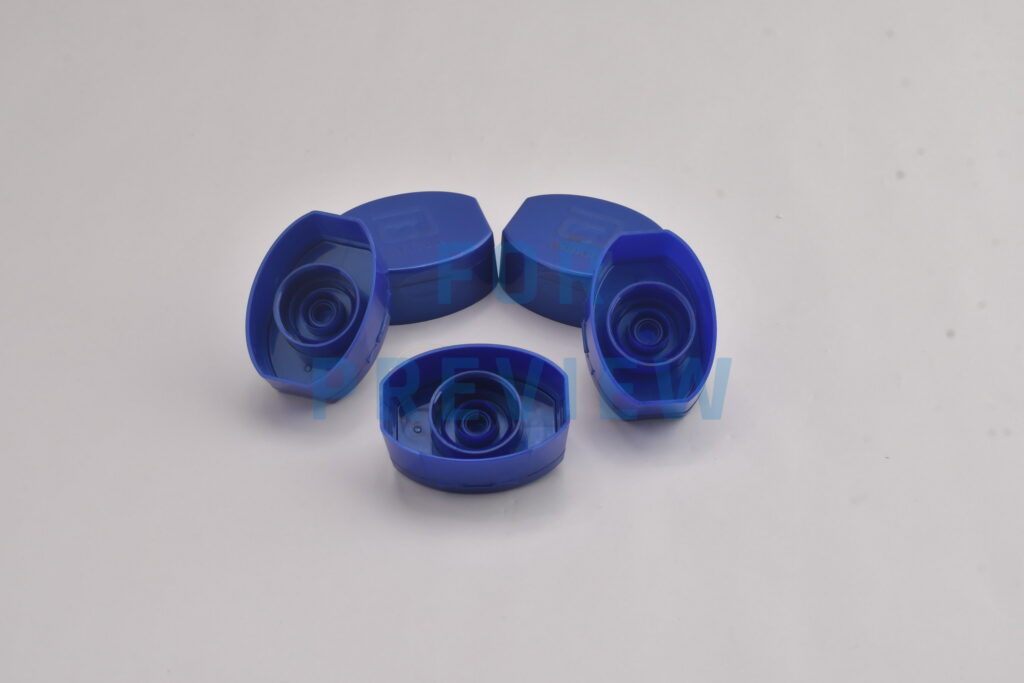
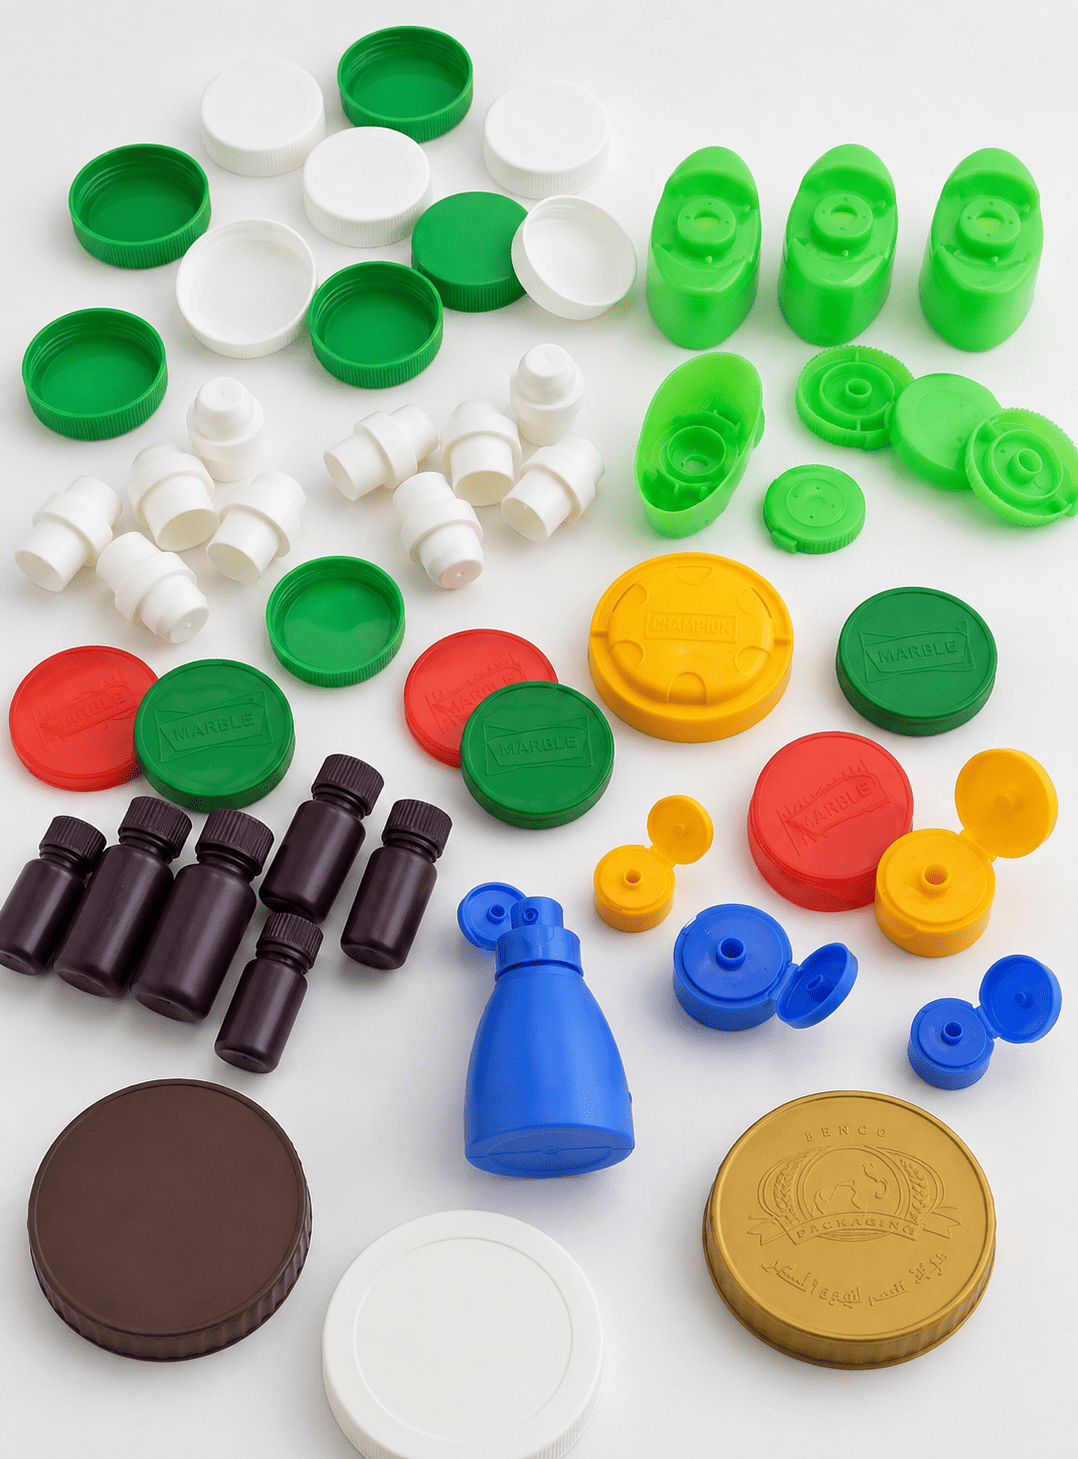
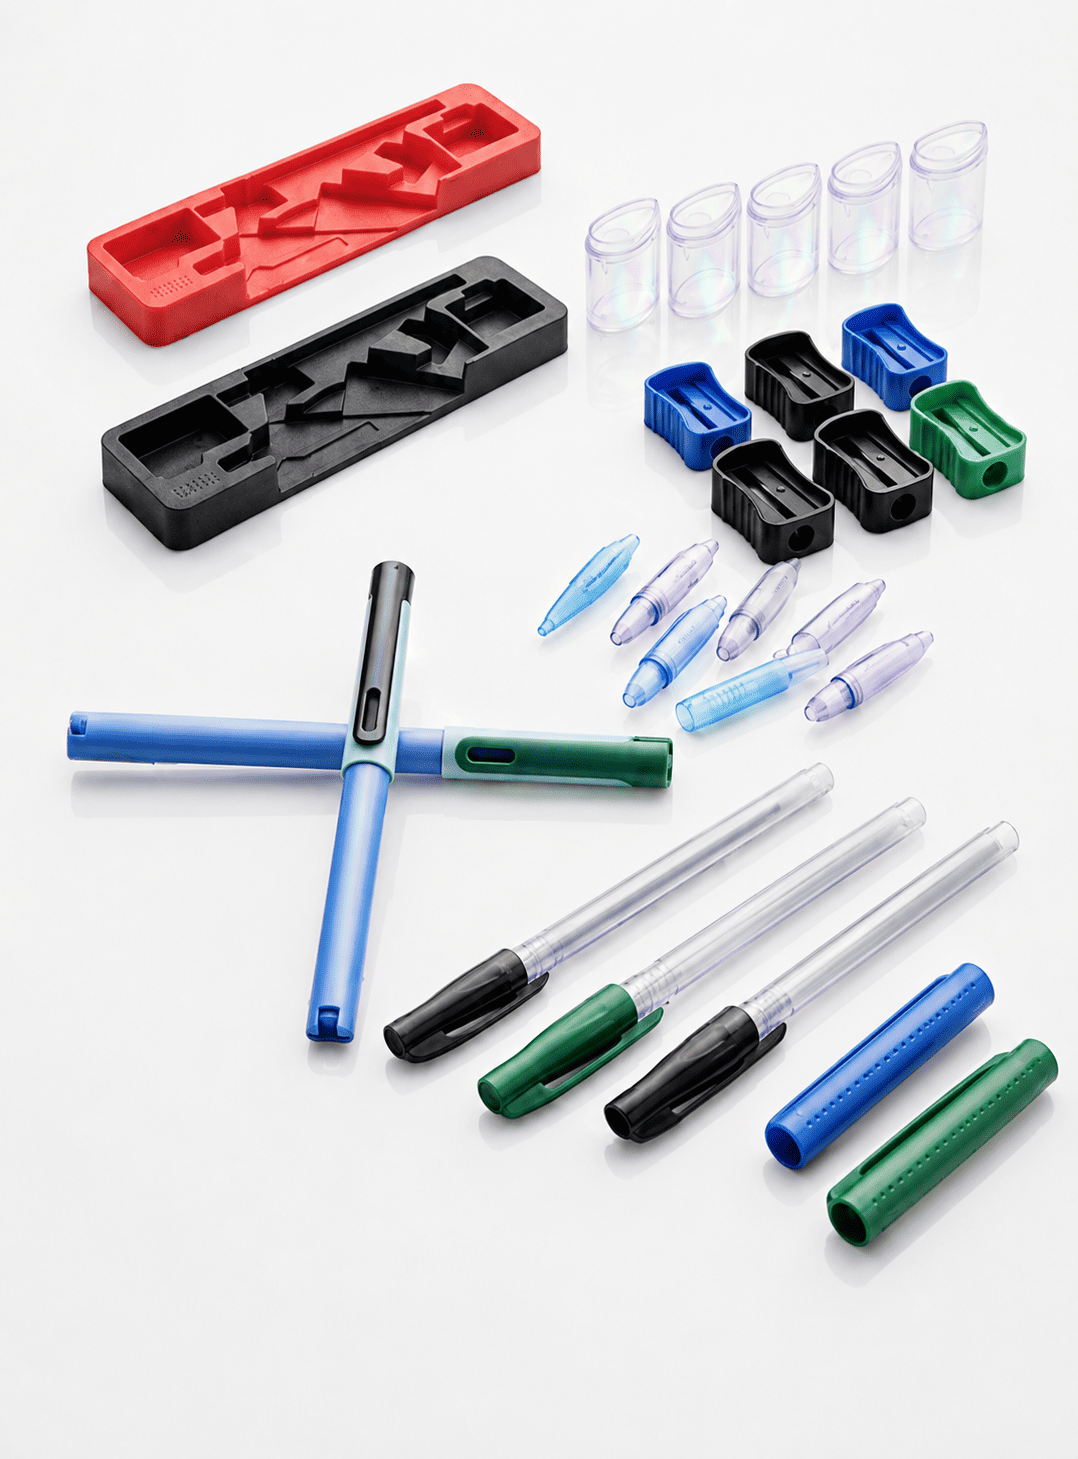
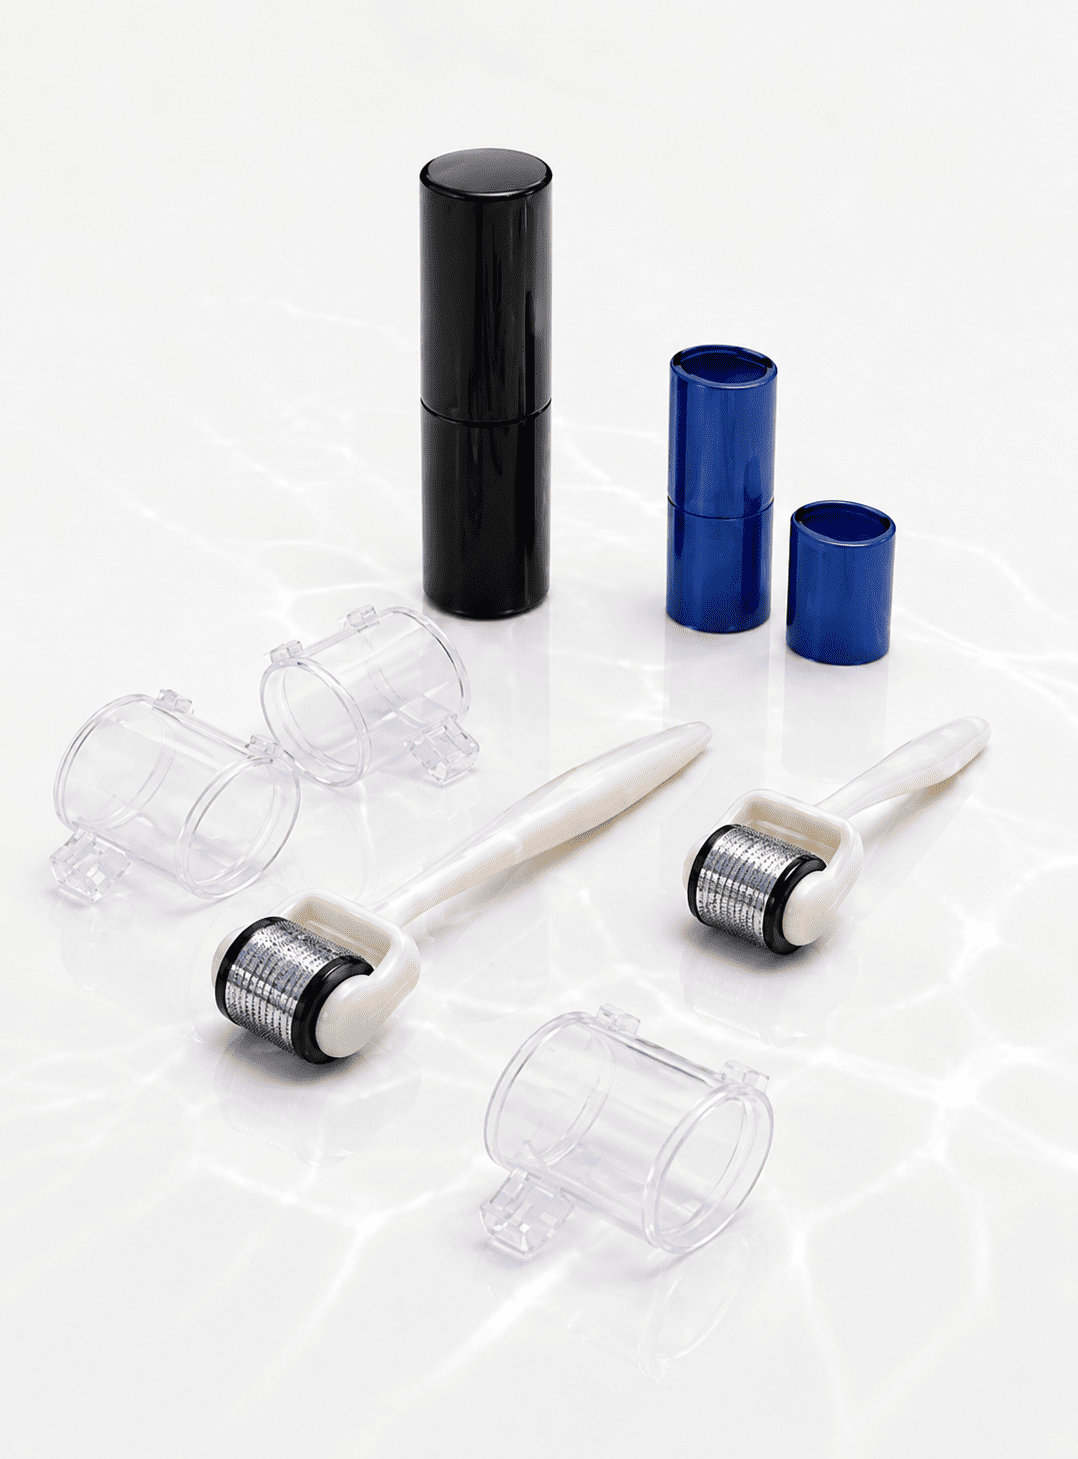
Our caps range is engineered for precision sealing, hygienic dispensing, and reliable protection in medical, pharmaceutical, and diagnostic applications. Manufactured using high-quality medical-grade polymers, these caps are designed to deliver leak-proof performance, user convenience, and dependable functionality in regulated healthcare environments.
Developed to support a wide variety of bottles, tubes, and container systems, our caps ensure consistent fitment and smooth operation across high-speed production lines. With strong focus on dimensional accuracy and material integrity, our products help maintain product safety, shelf life, and packaging efficiency in critical applications.
Key Features
We utilize certified medical-grade raw materials that support safety, chemical compatibility, and long-term reliability. The caps are engineered for secure and leak-proof sealing performance, helping protect sensitive formulations during storage and transportation. Precision molding ensures high dimensional accuracy and consistent thread engagement for dependable closure performance.
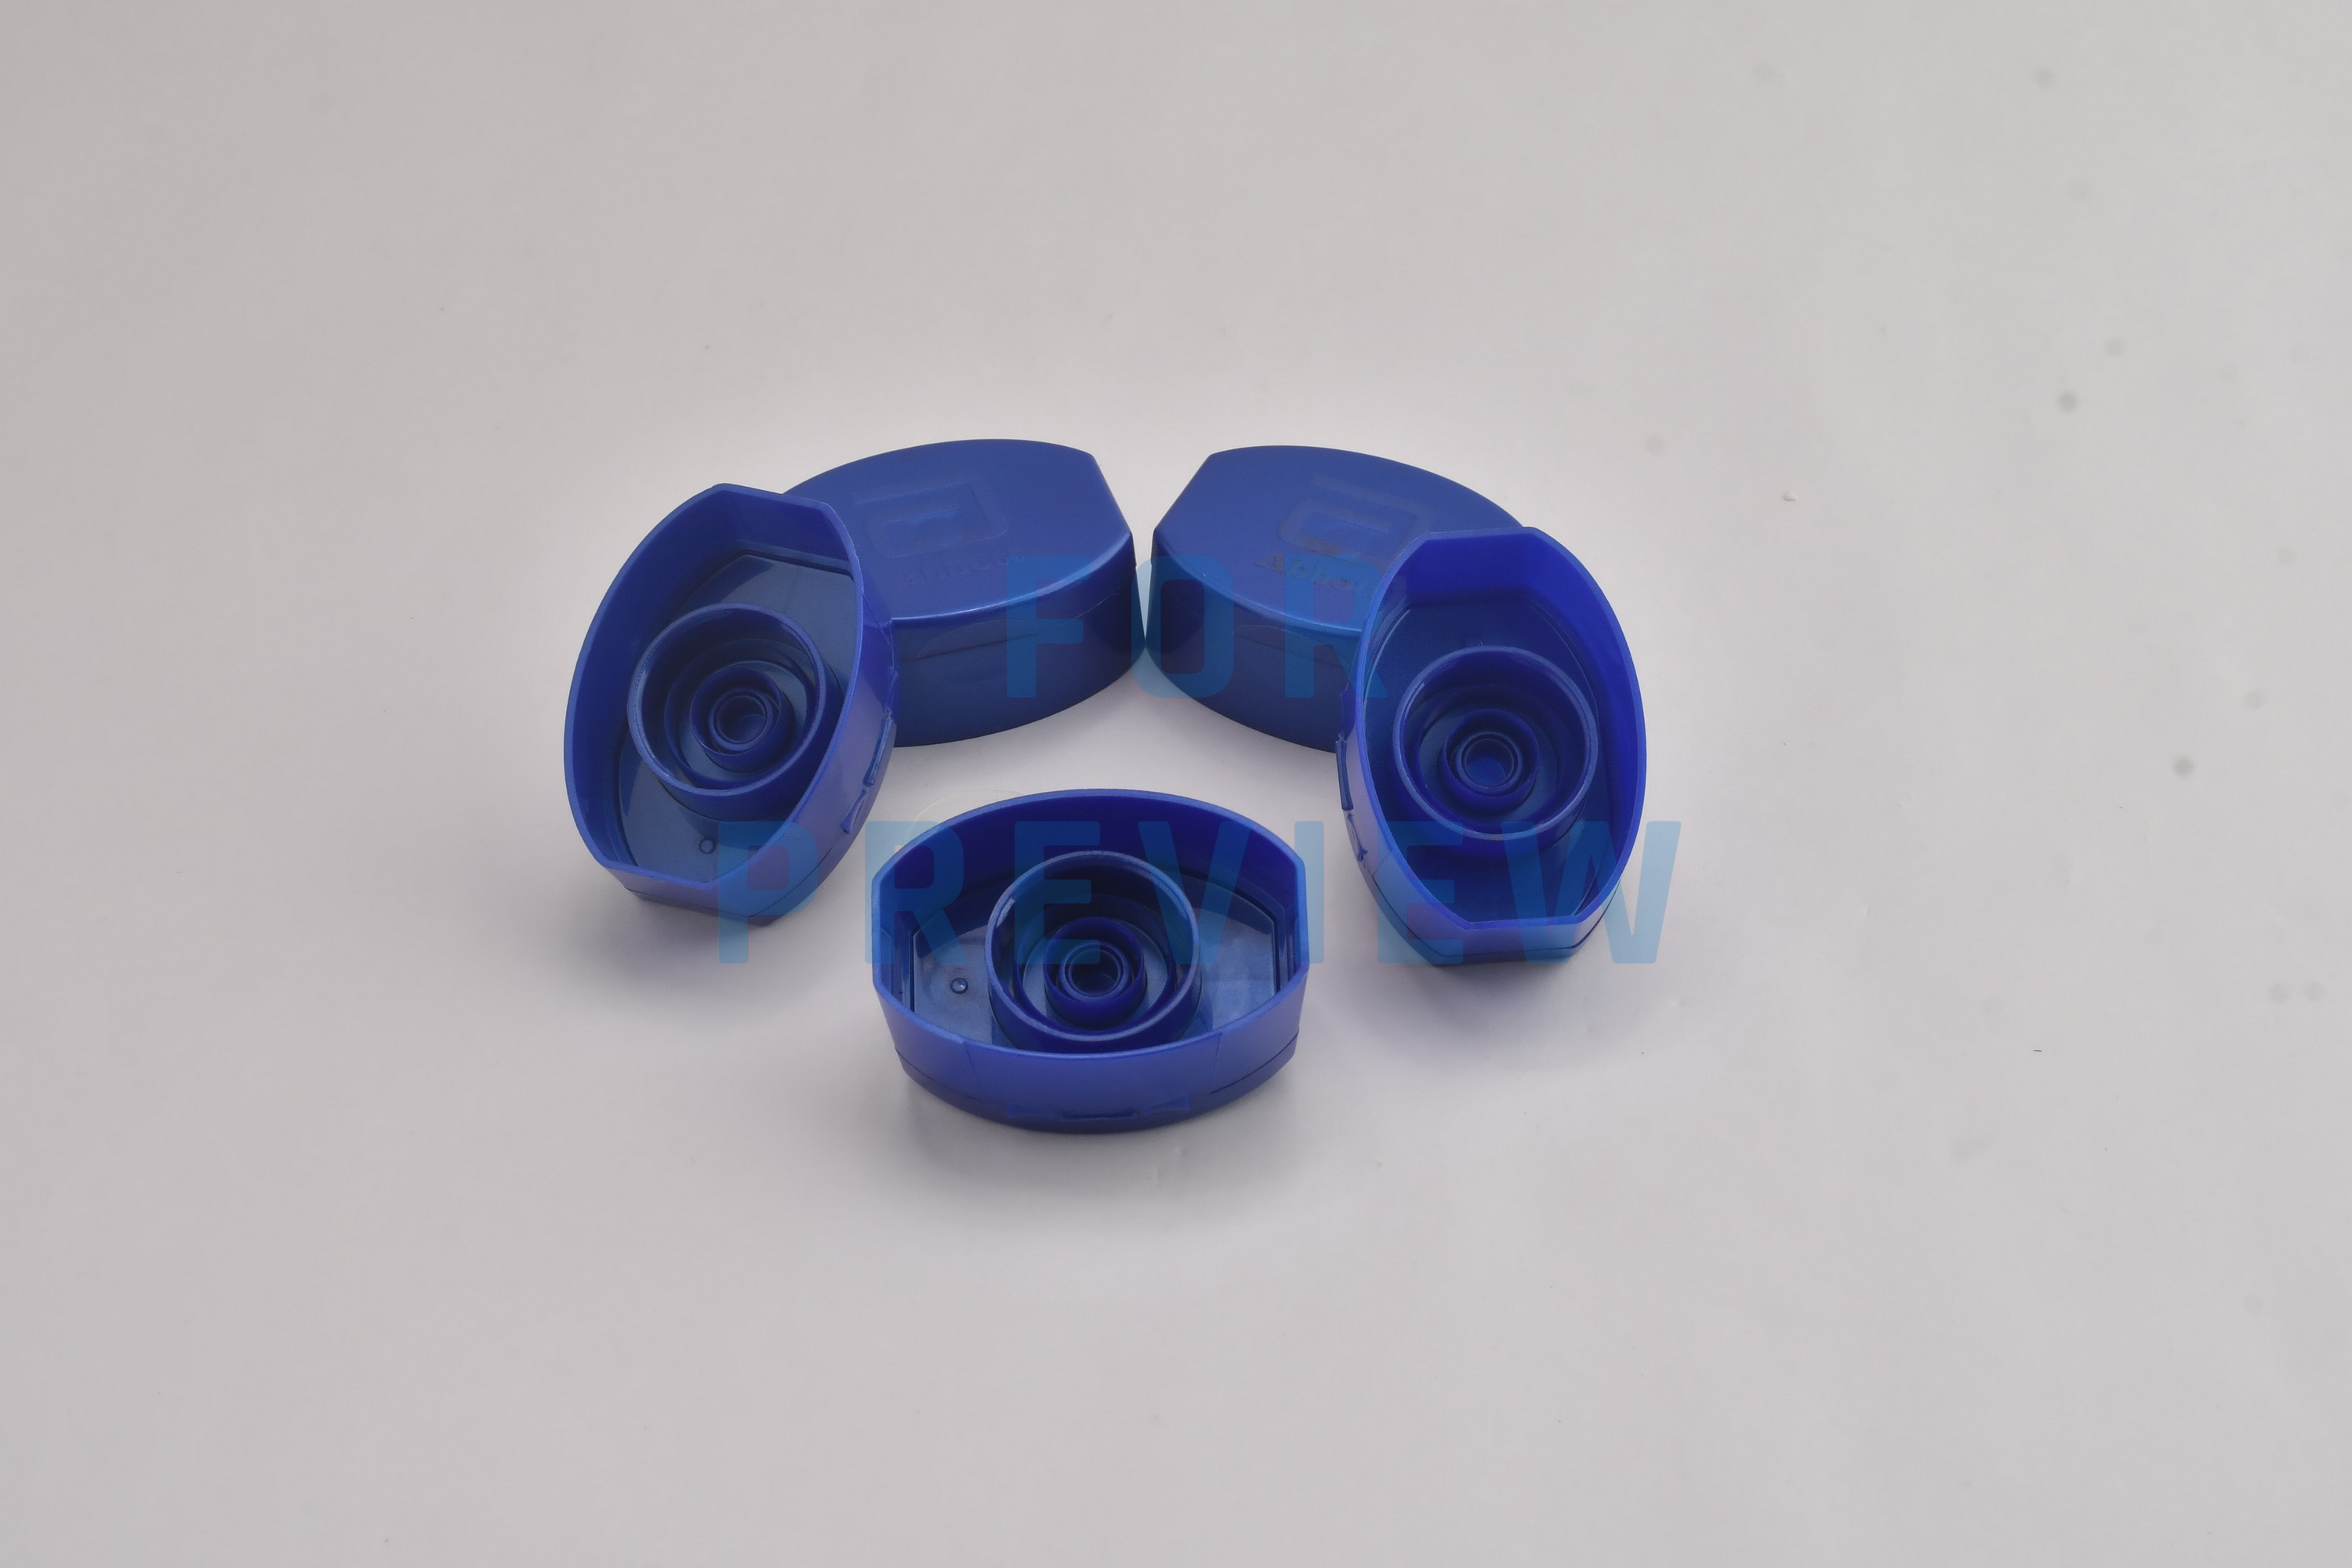
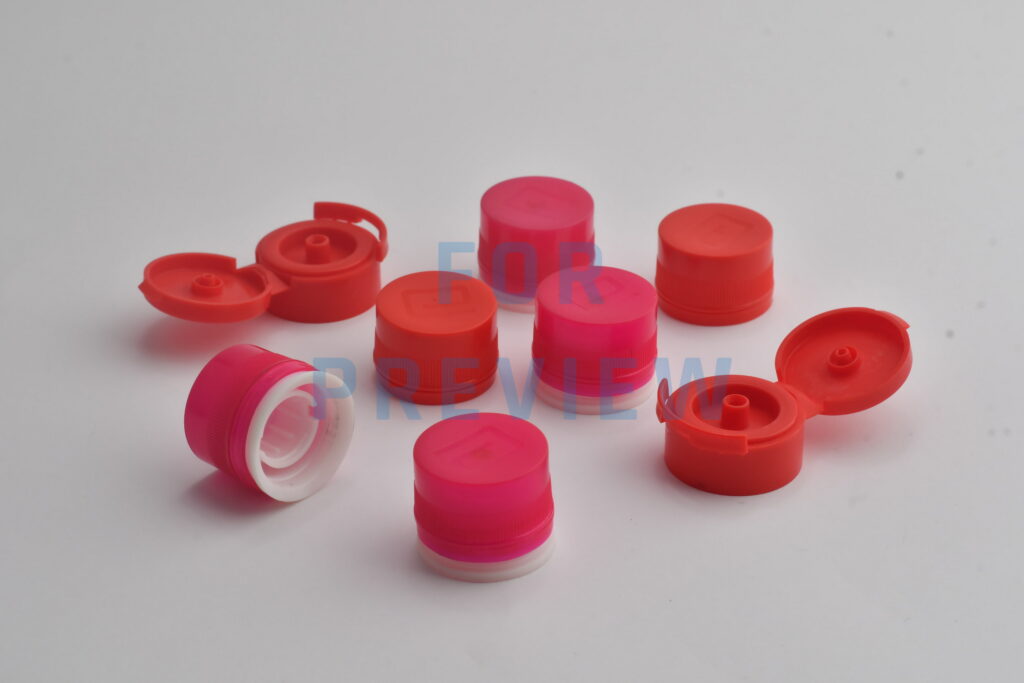
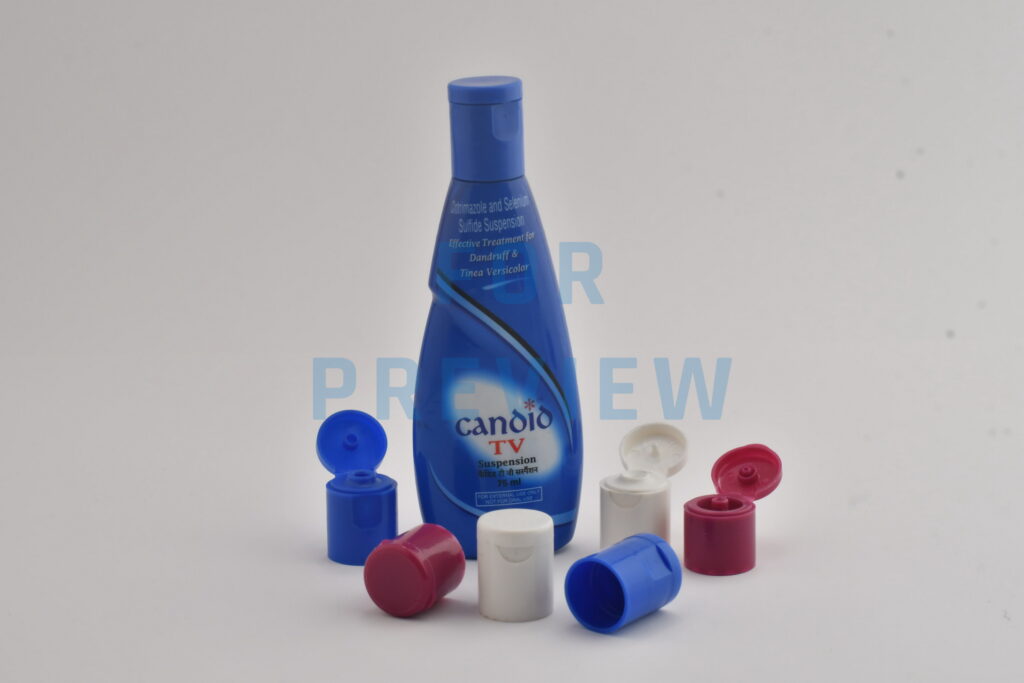
Each component is produced with a smooth flip and closure mechanism that enhances user convenience and functional reliability. Tamper-evident design options are available to support product security and regulatory requirements. Our caps are compatible with automated filling and capping lines, enabling efficient large-scale production, and can be supplied in custom colors and branding configurations to meet specific customer requirements.
Product Range Under Caps
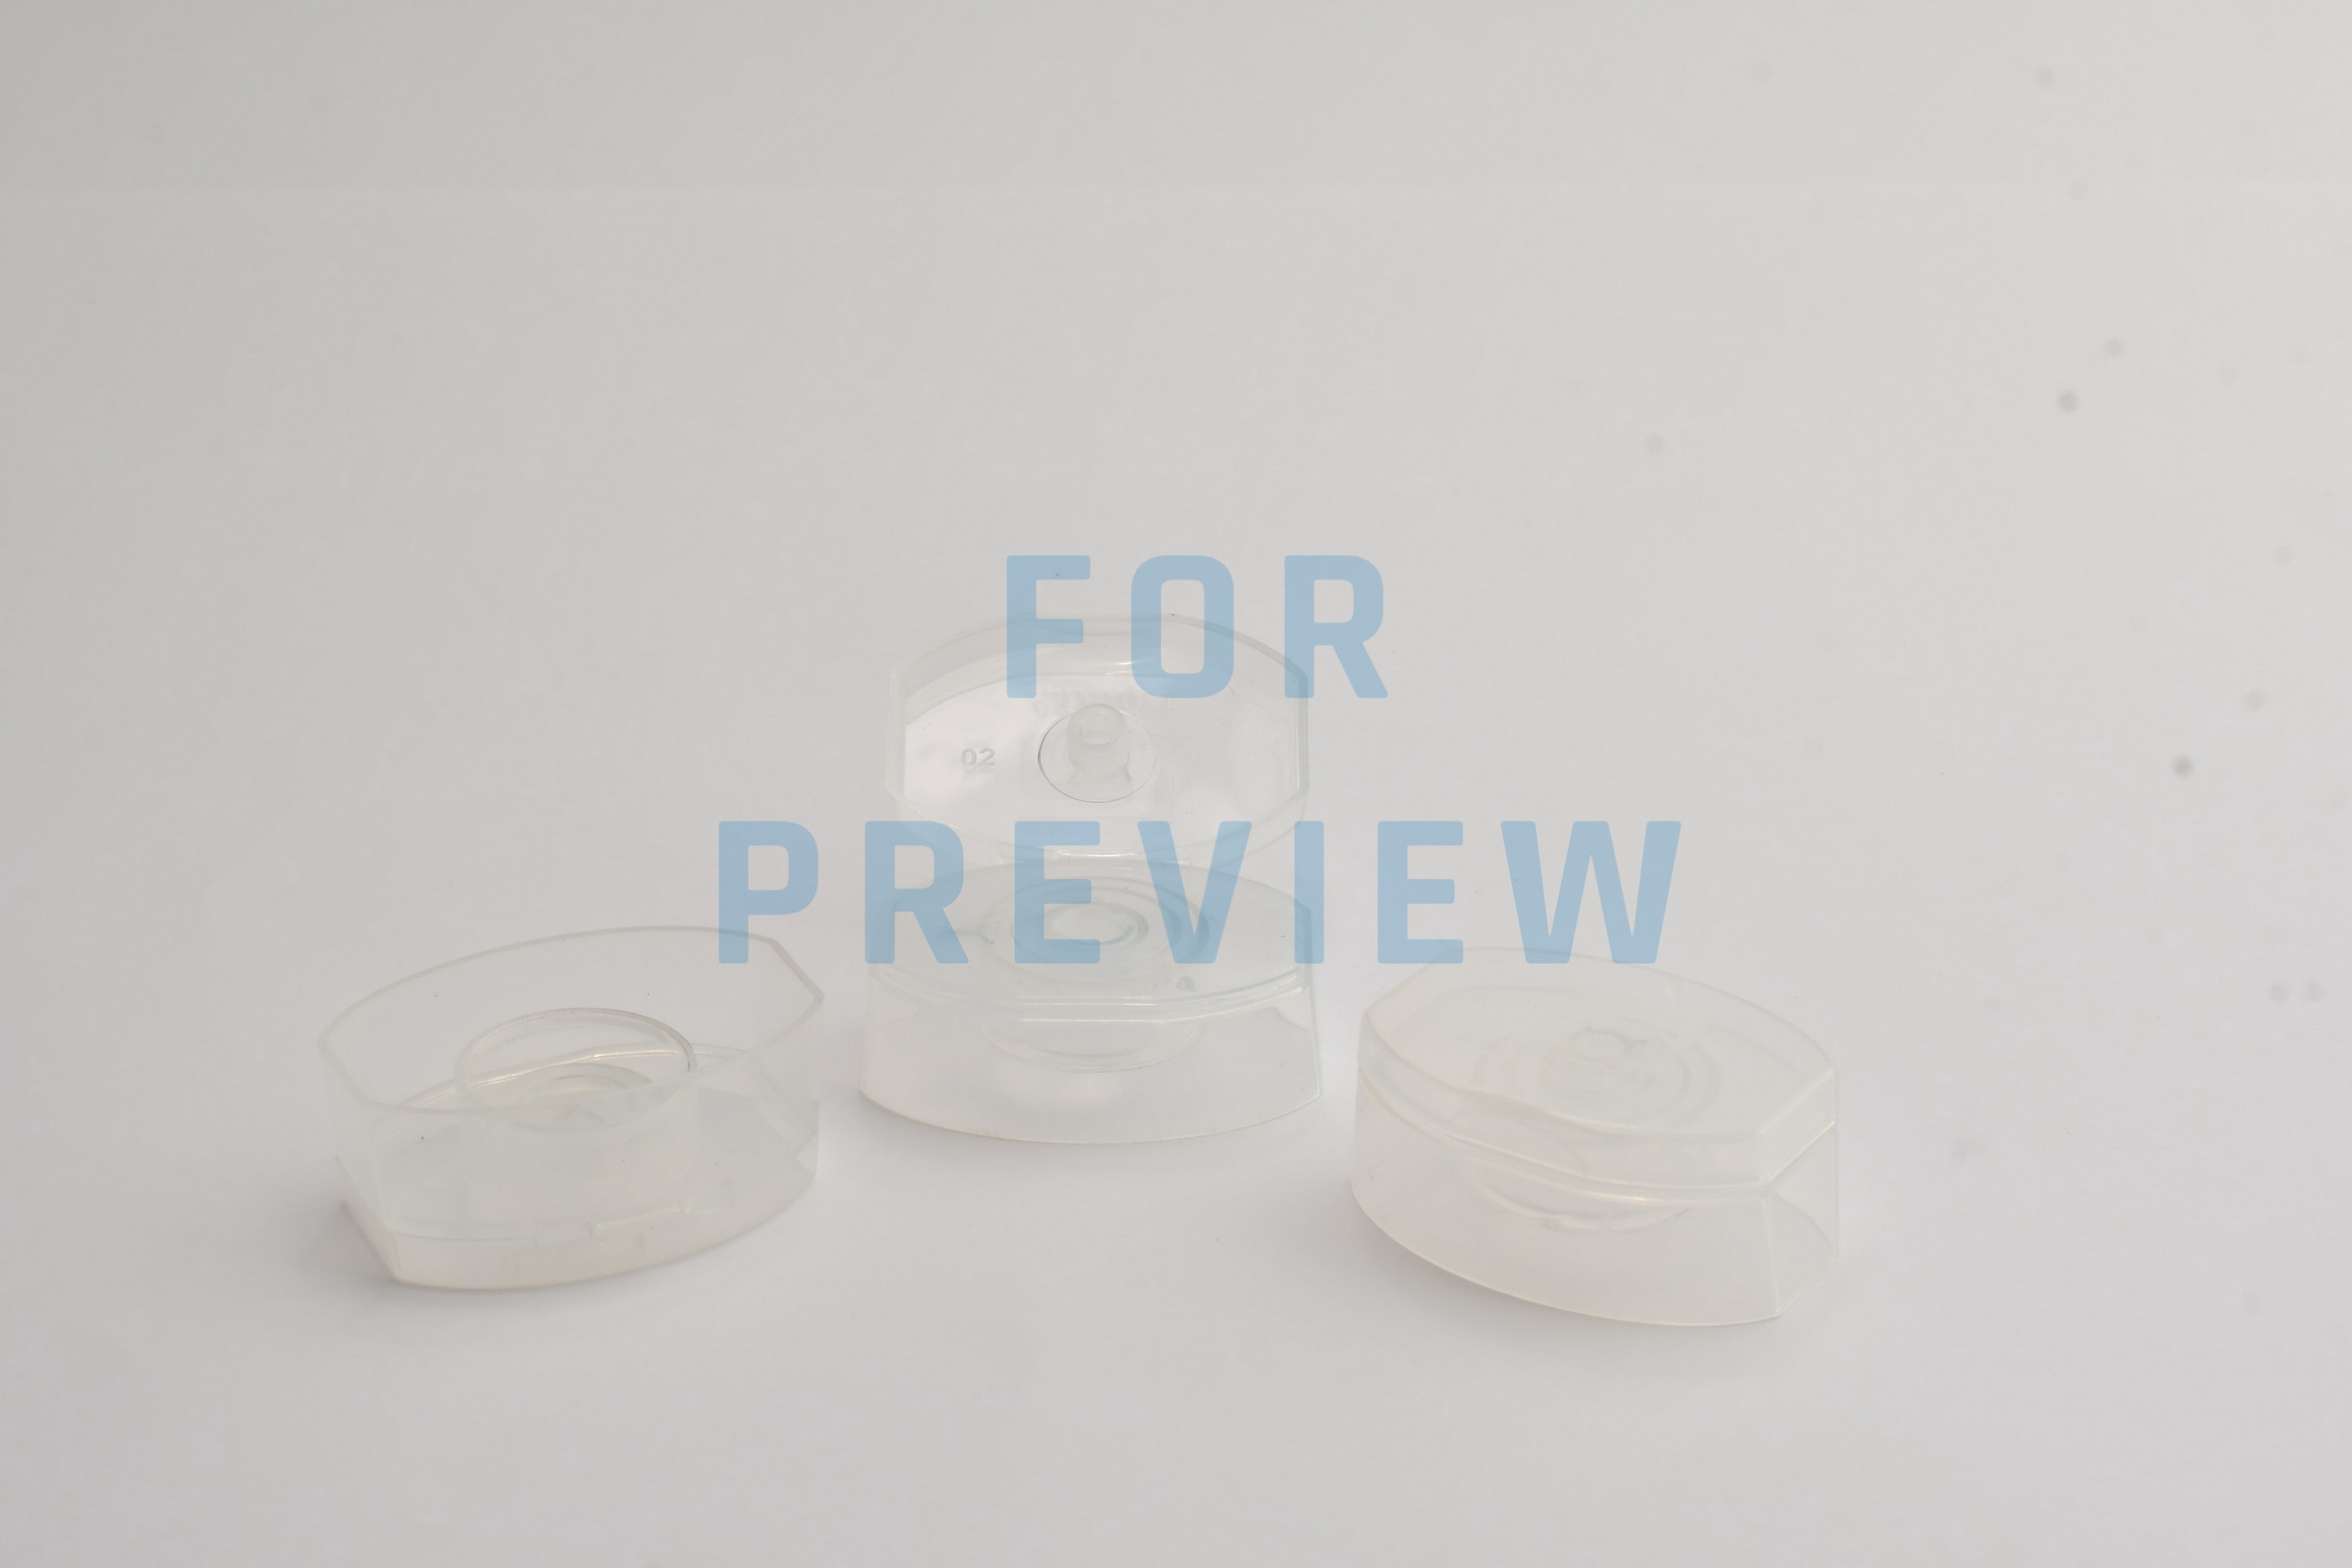
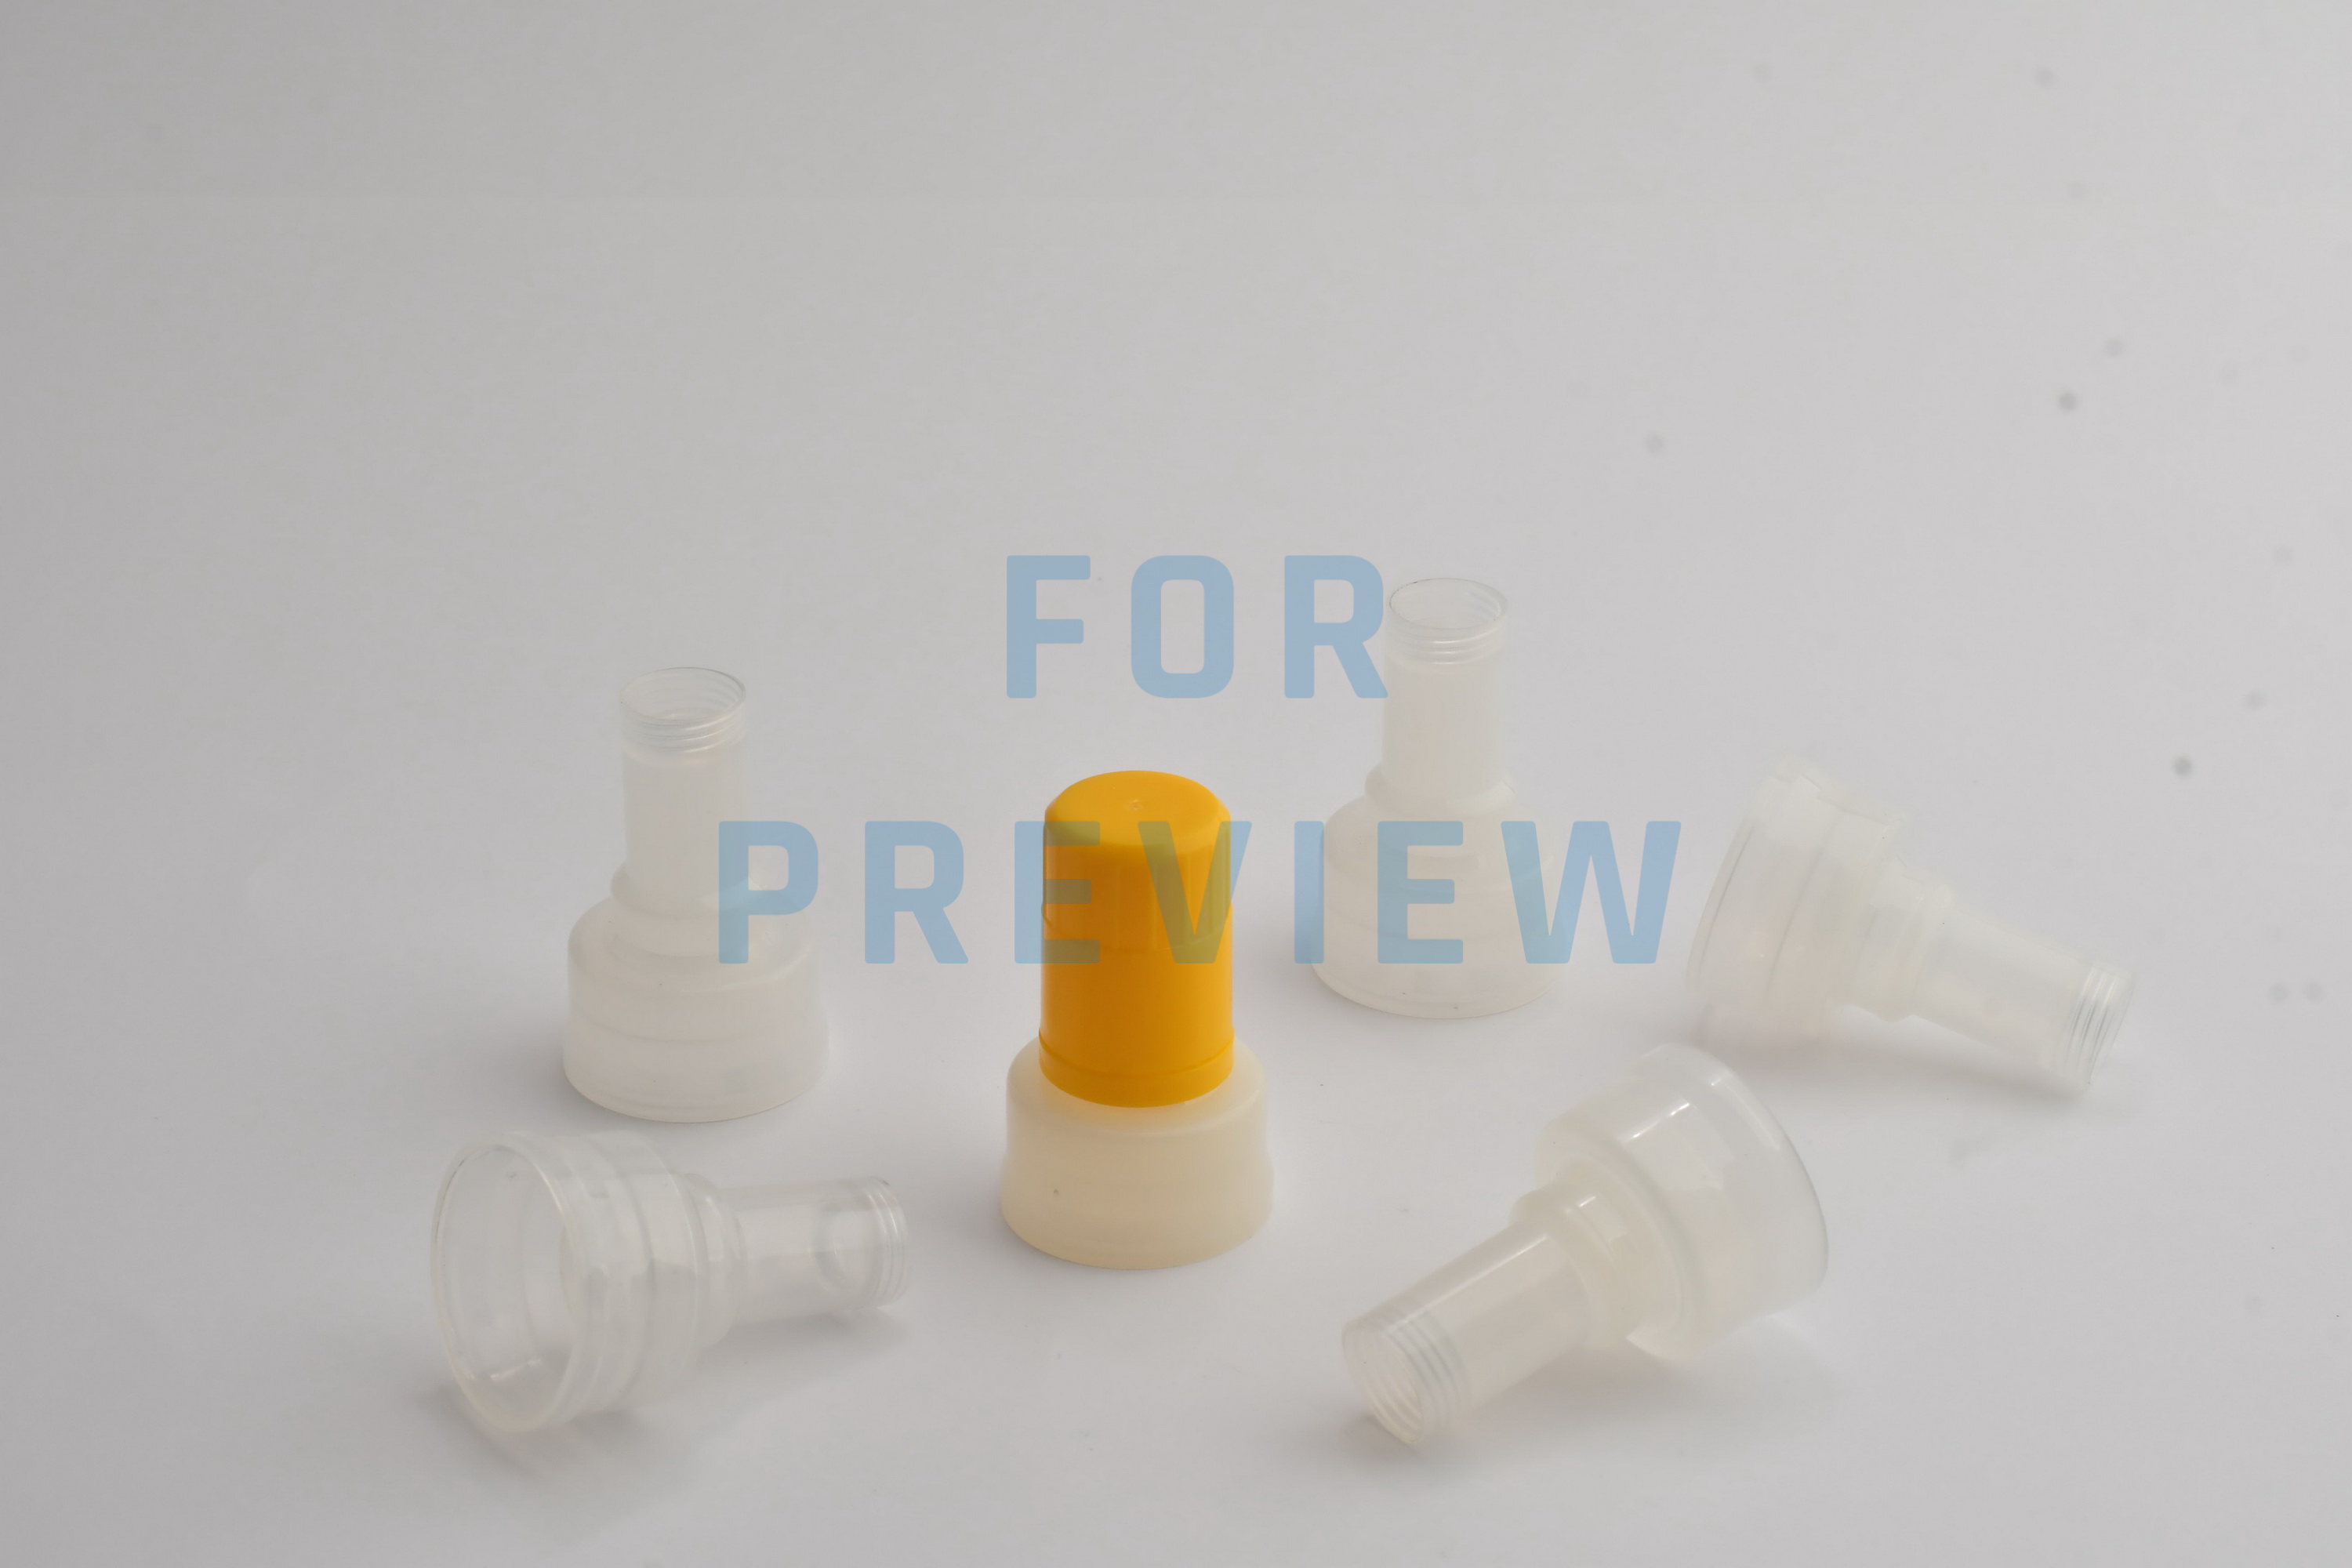
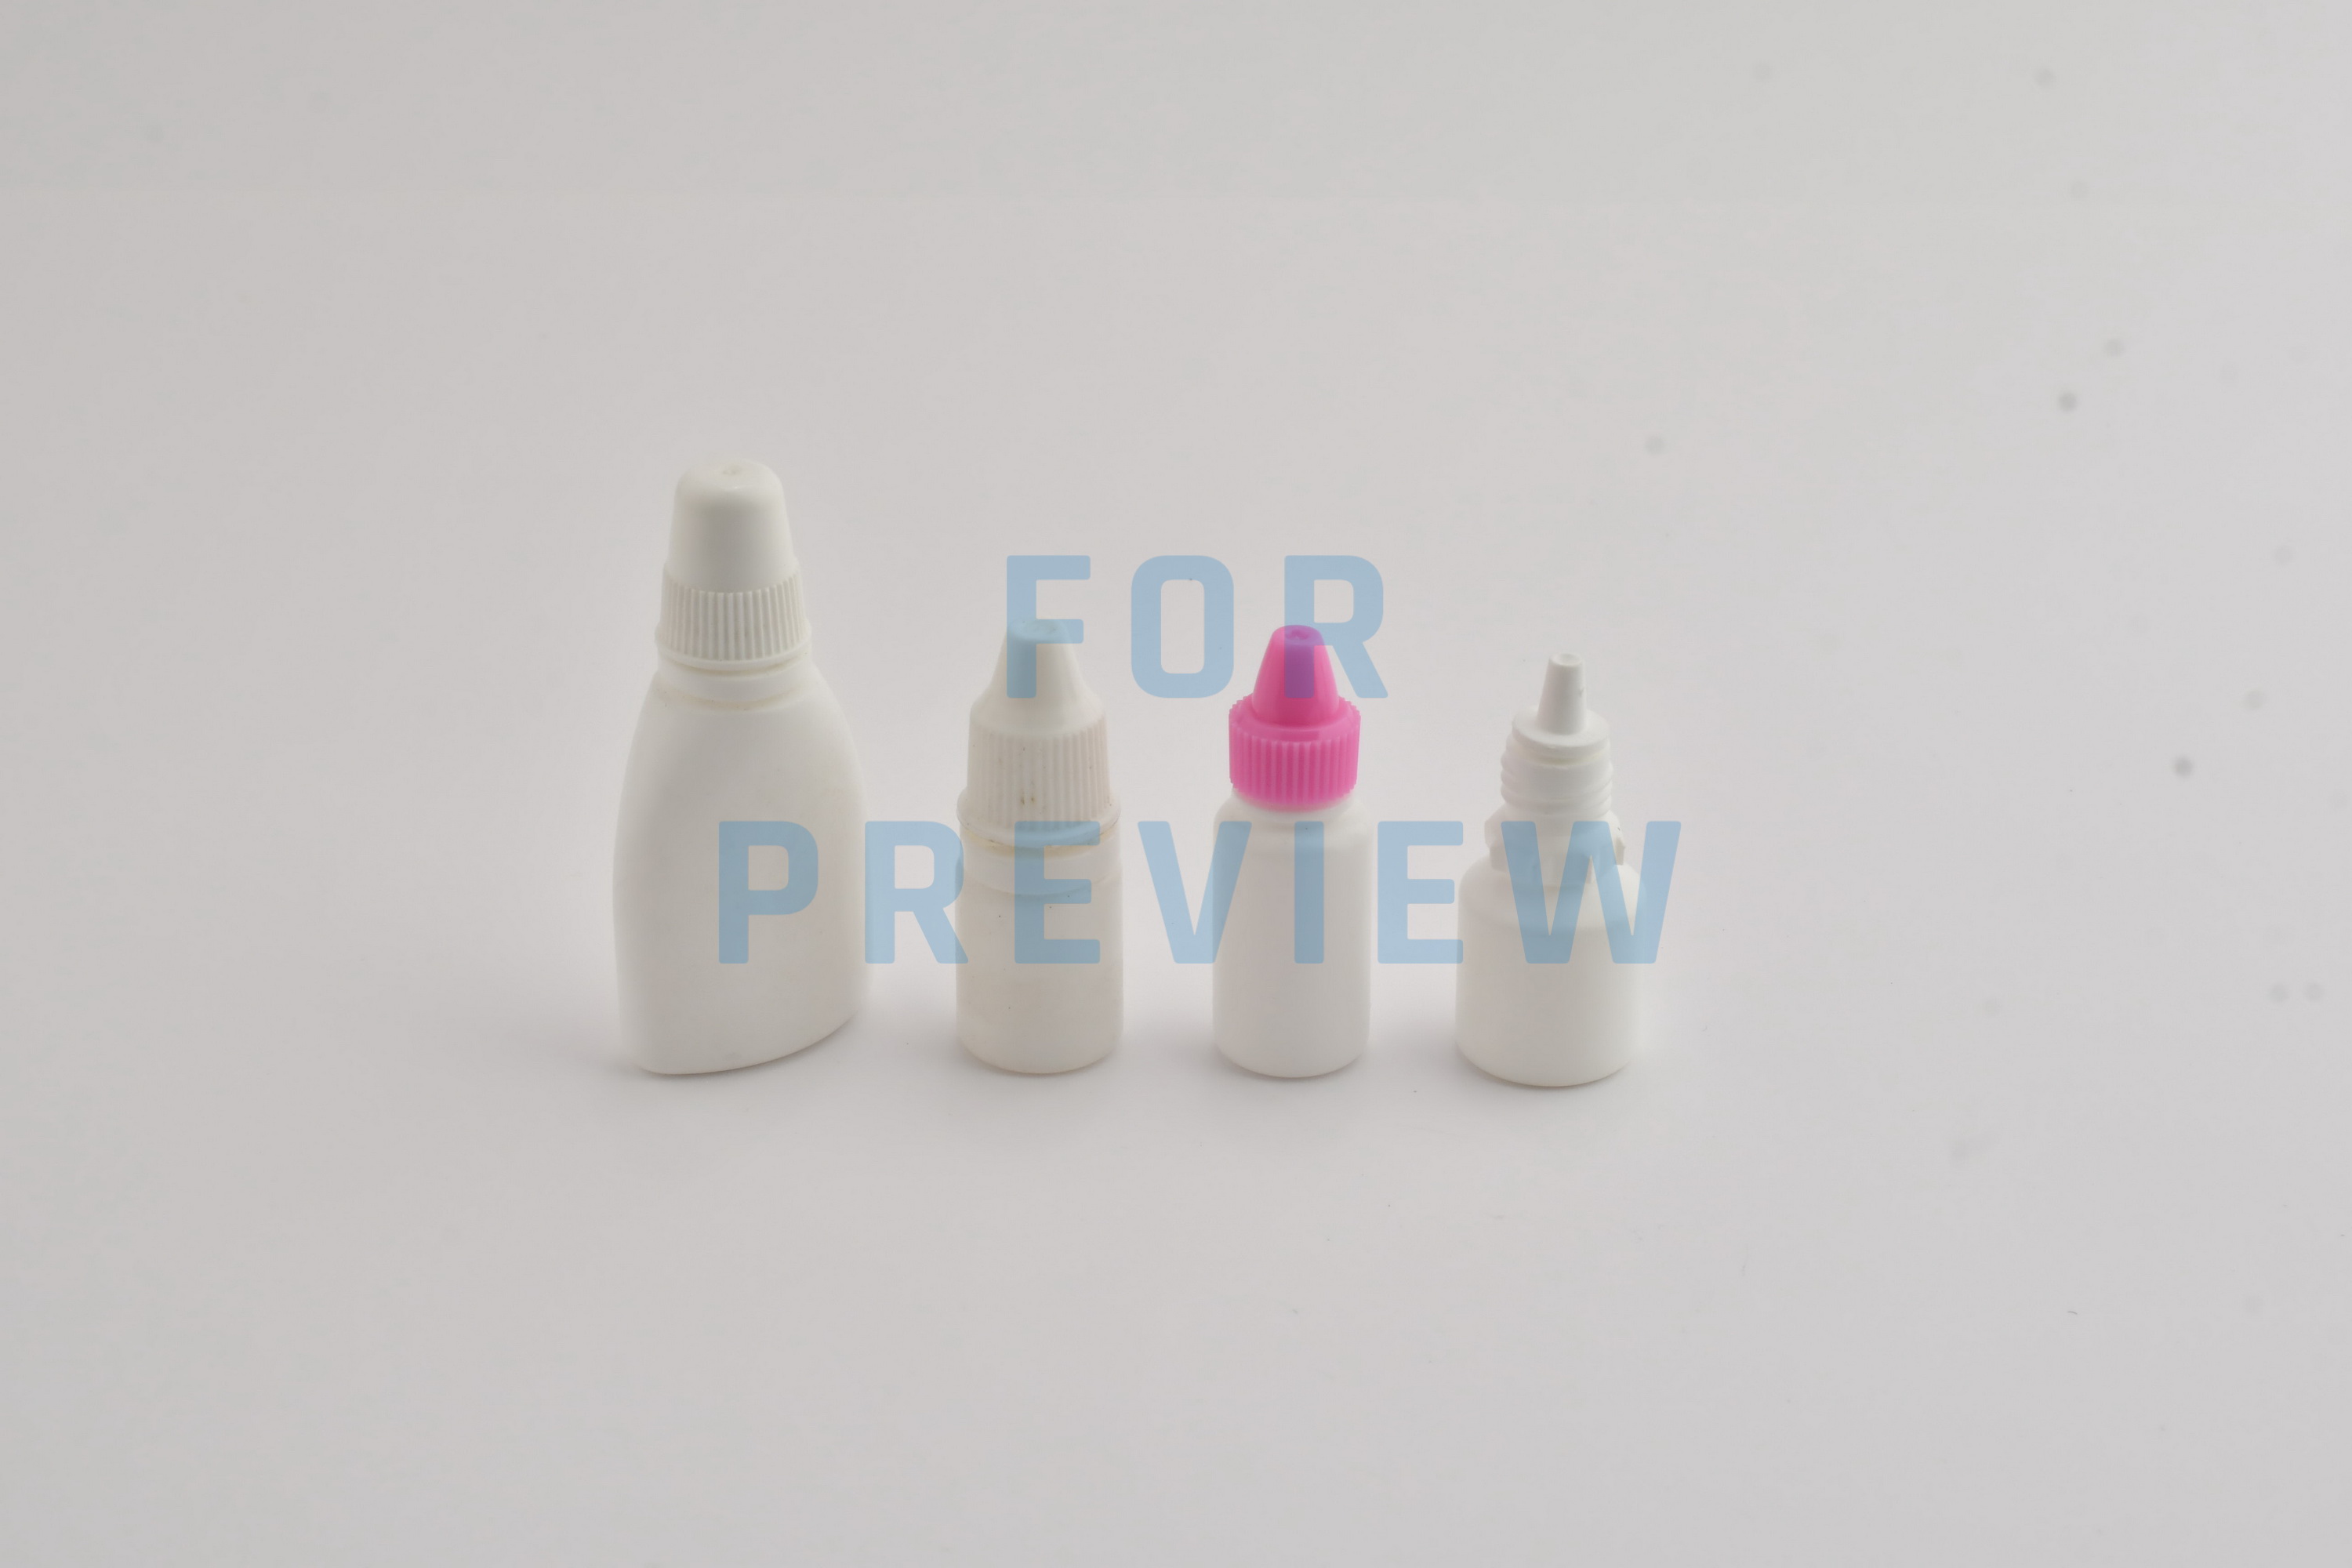
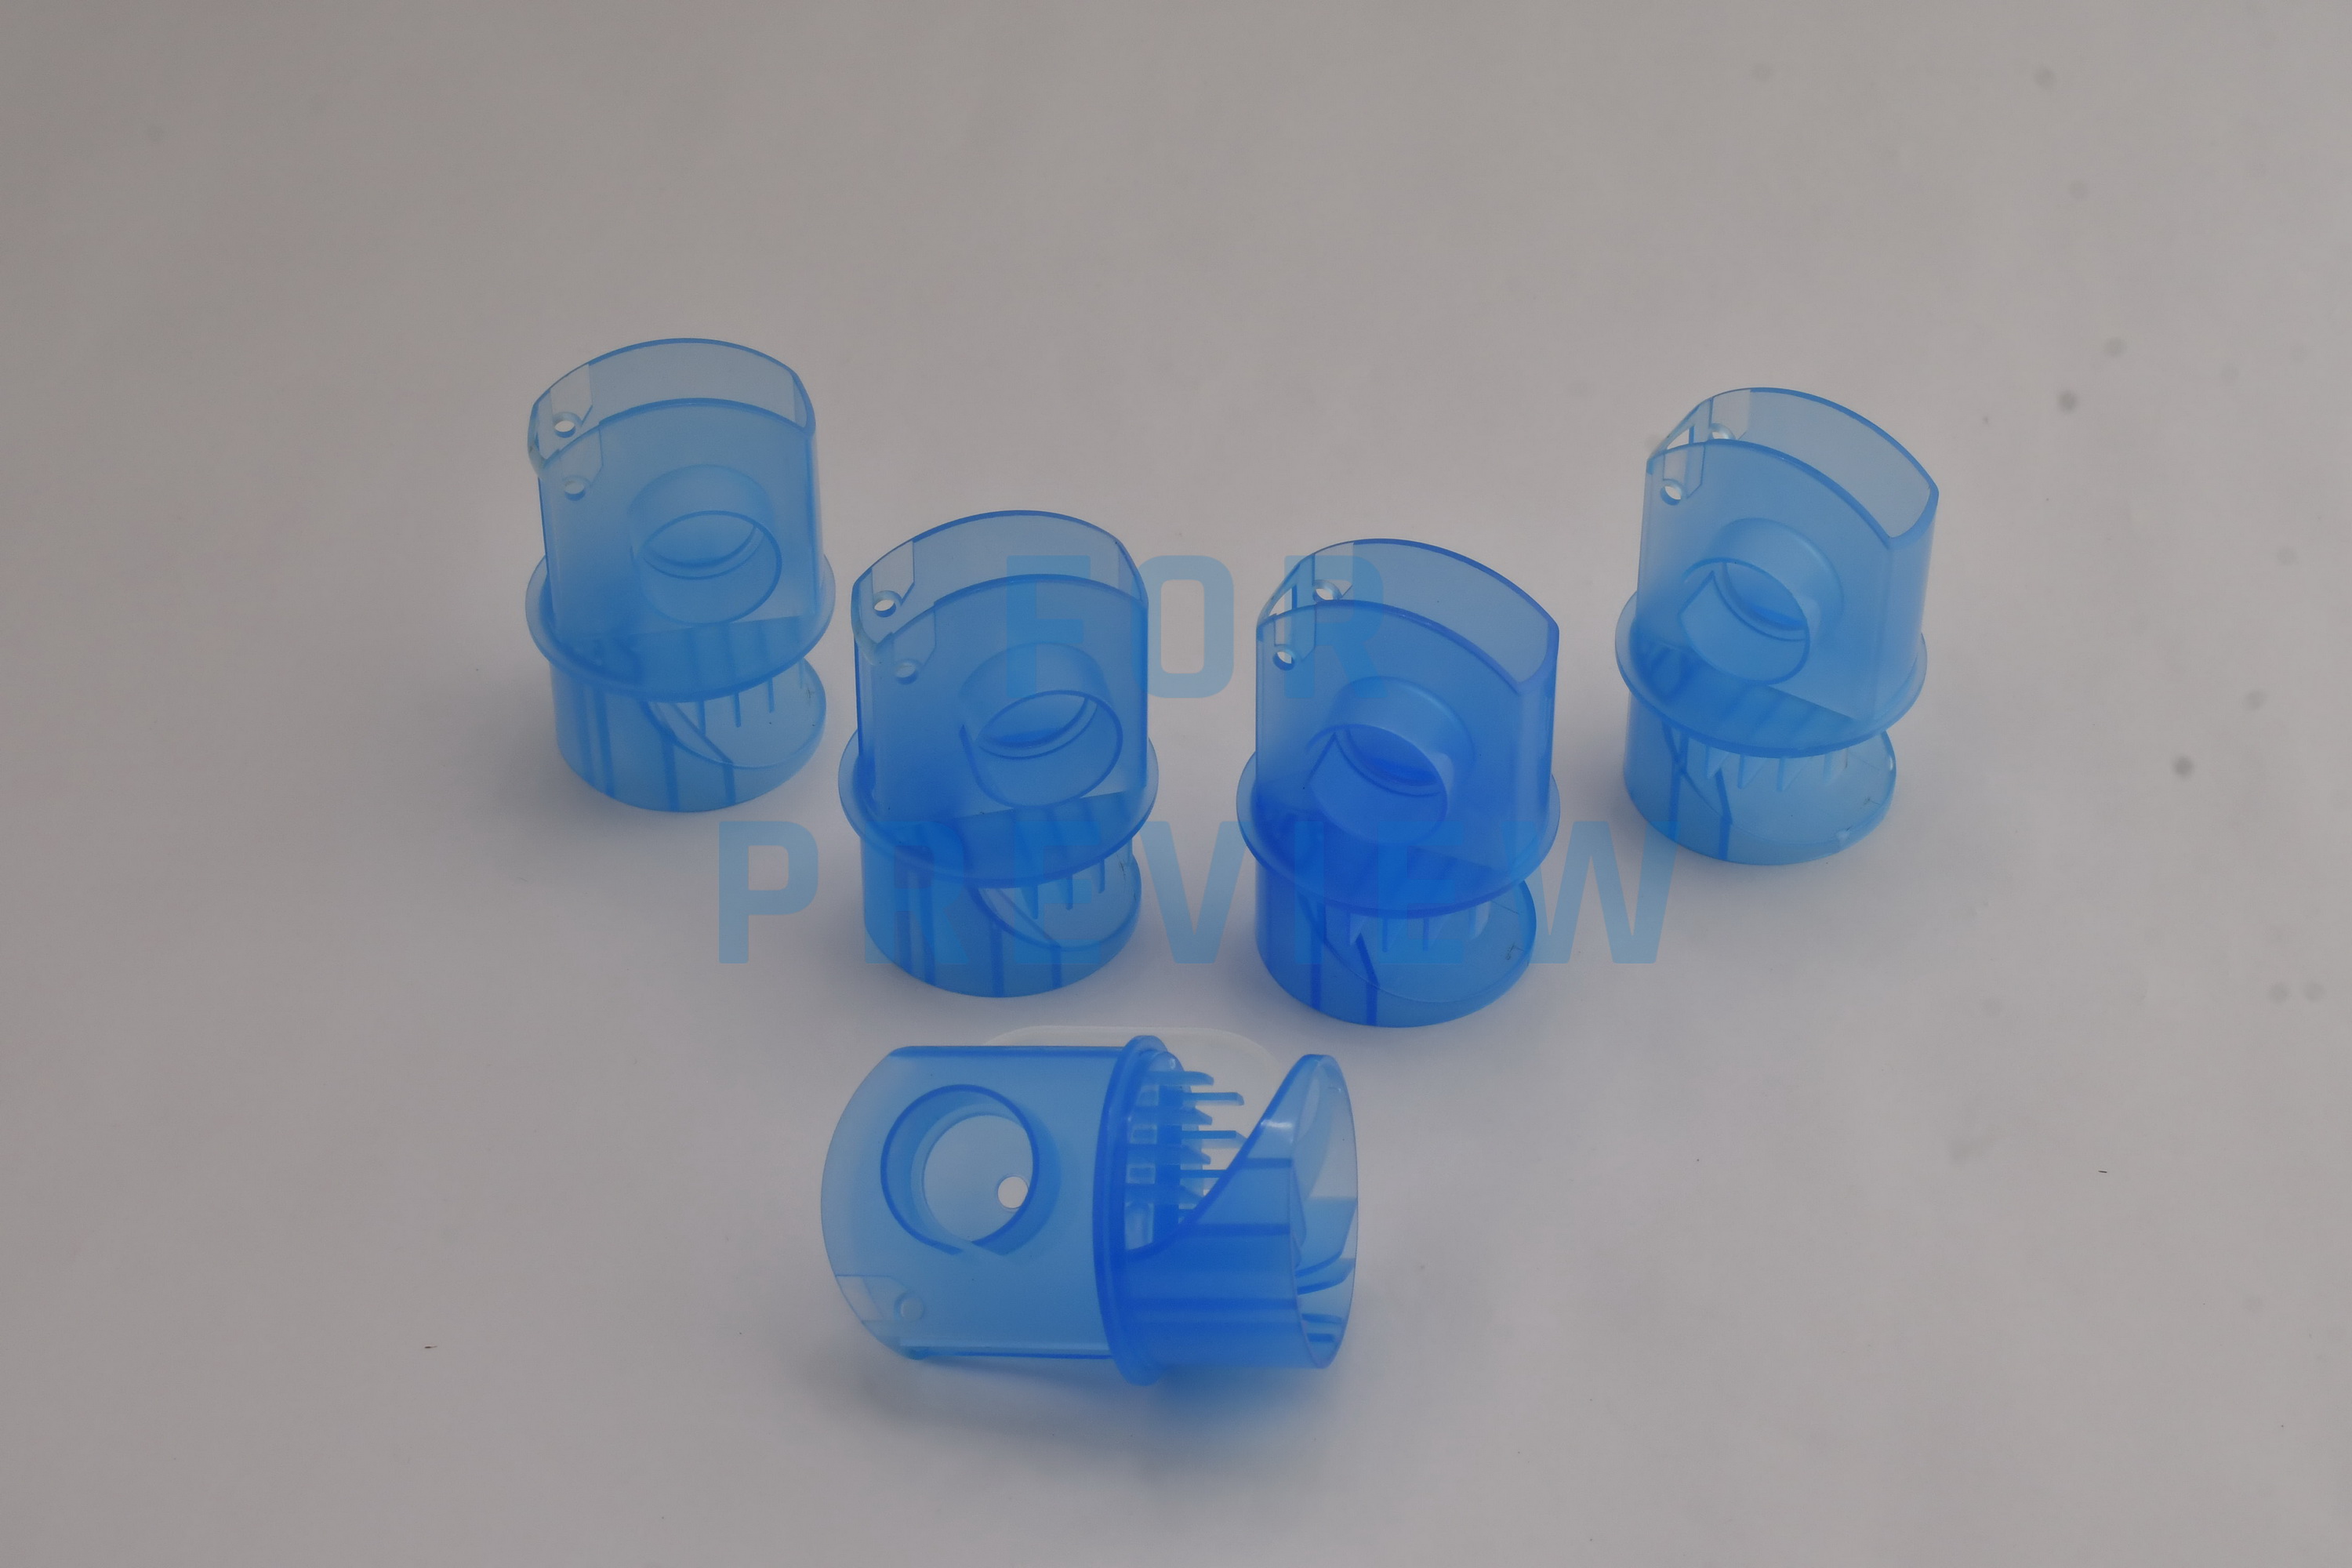
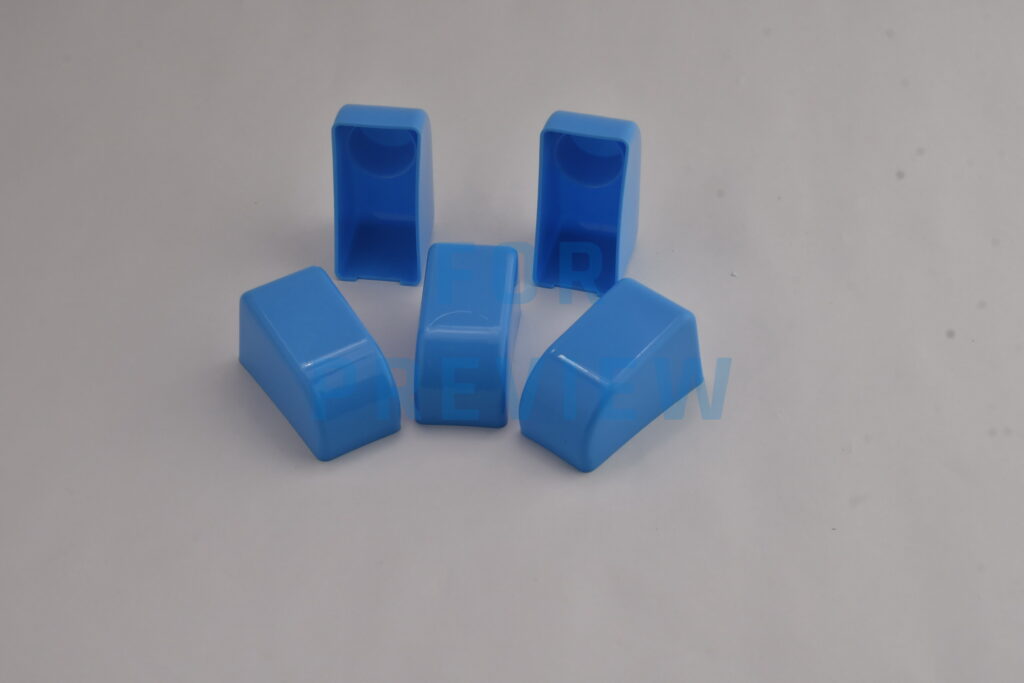
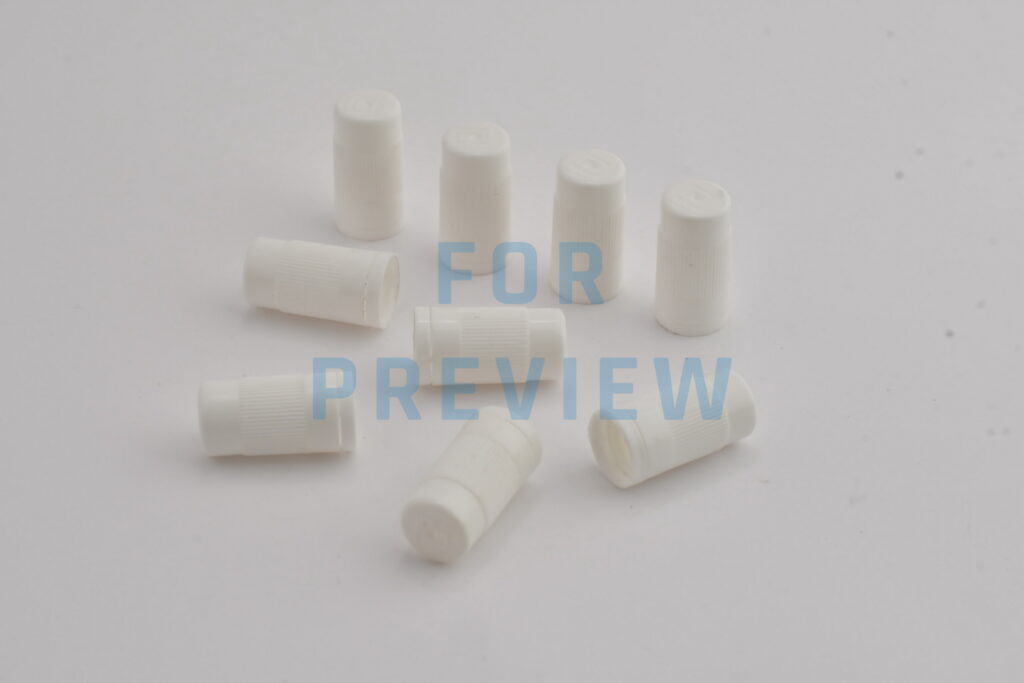
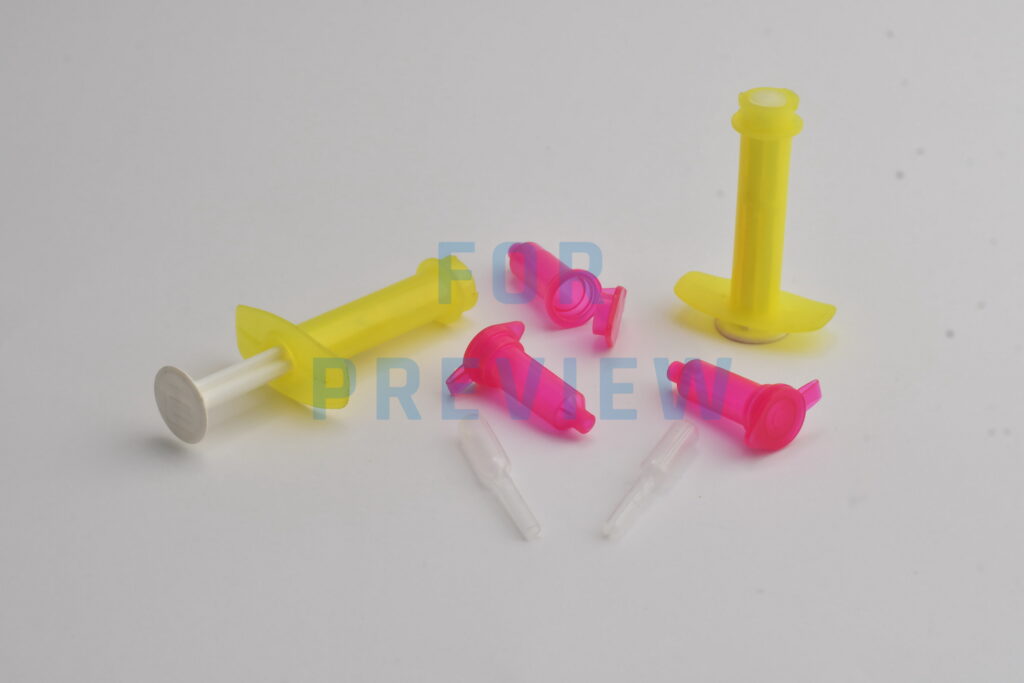
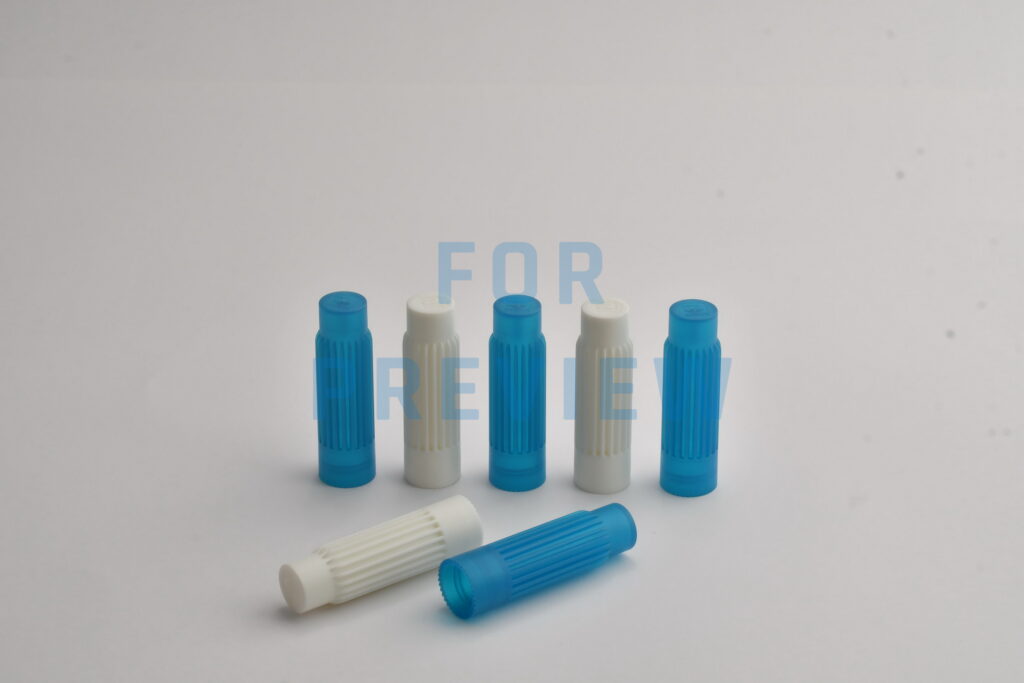
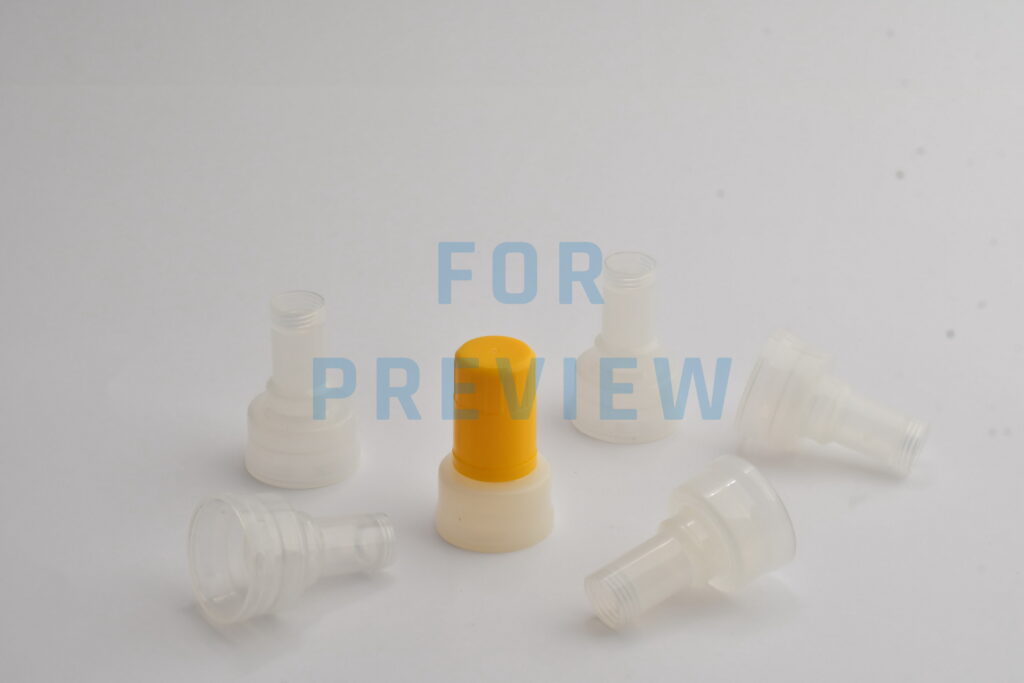
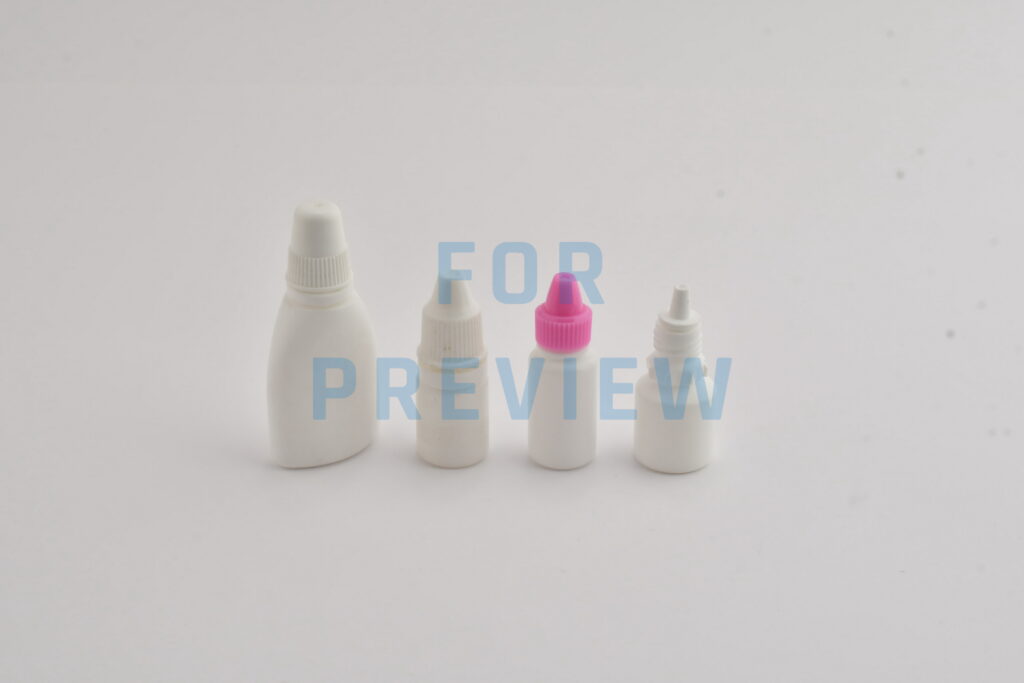
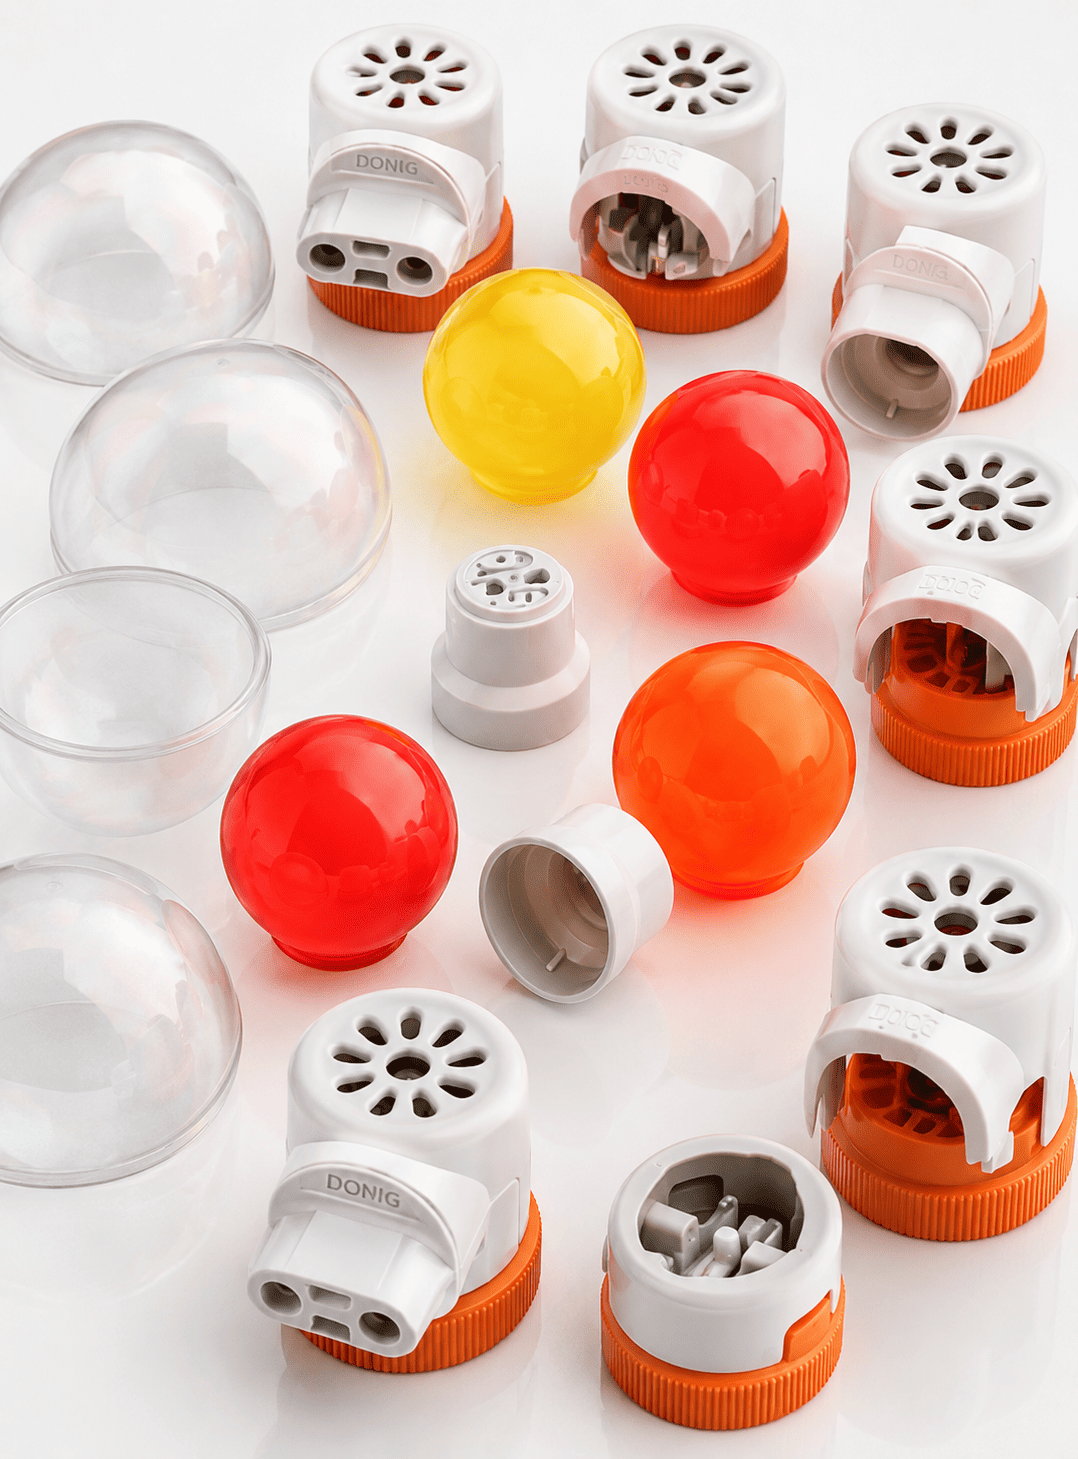
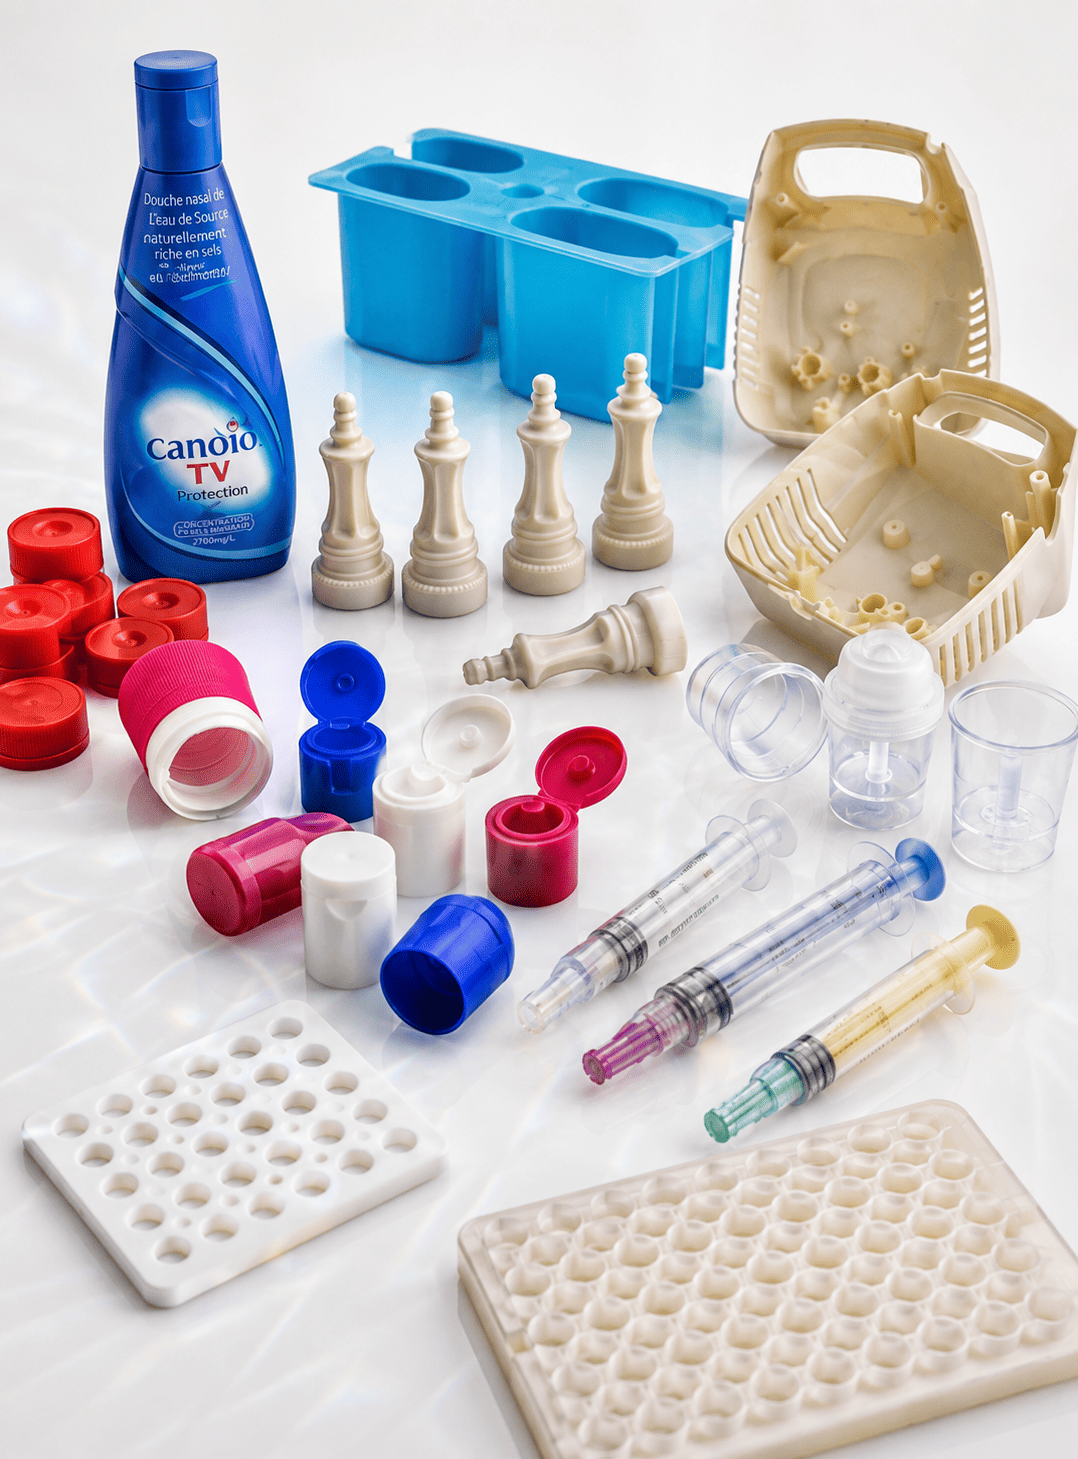
Our caps portfolio includes a comprehensive range of solutions such as flip top caps designed for convenient dispensing, actuator caps developed for controlled delivery systems, and nasivision caps engineered for nasal applications. We also manufacture adaptor caps and retrofit caps that support secure integration with specialized container systems.
The range further includes paediatrics caps designed with safety and usability in mind, soft tip caps for controlled application, tube caps for secure sealing of flexible packaging, and case caps developed for protective and functional closure requirements across medical and pharmaceutical packaging lines.
Why Choose Our Caps?
Our caps are trusted for proven performance in medical and pharmaceutical applications where sealing reliability and product safety are critical. With advanced precision molding technology and strict quality control processes, we deliver consistent and dependable components.
Our scalable manufacturing capability ensures reliable supply for both growing and high-volume programs, while our competitive pricing and strong technical support help customers achieve efficient product integration and long-term value.